Wire
EDM
in Lodz
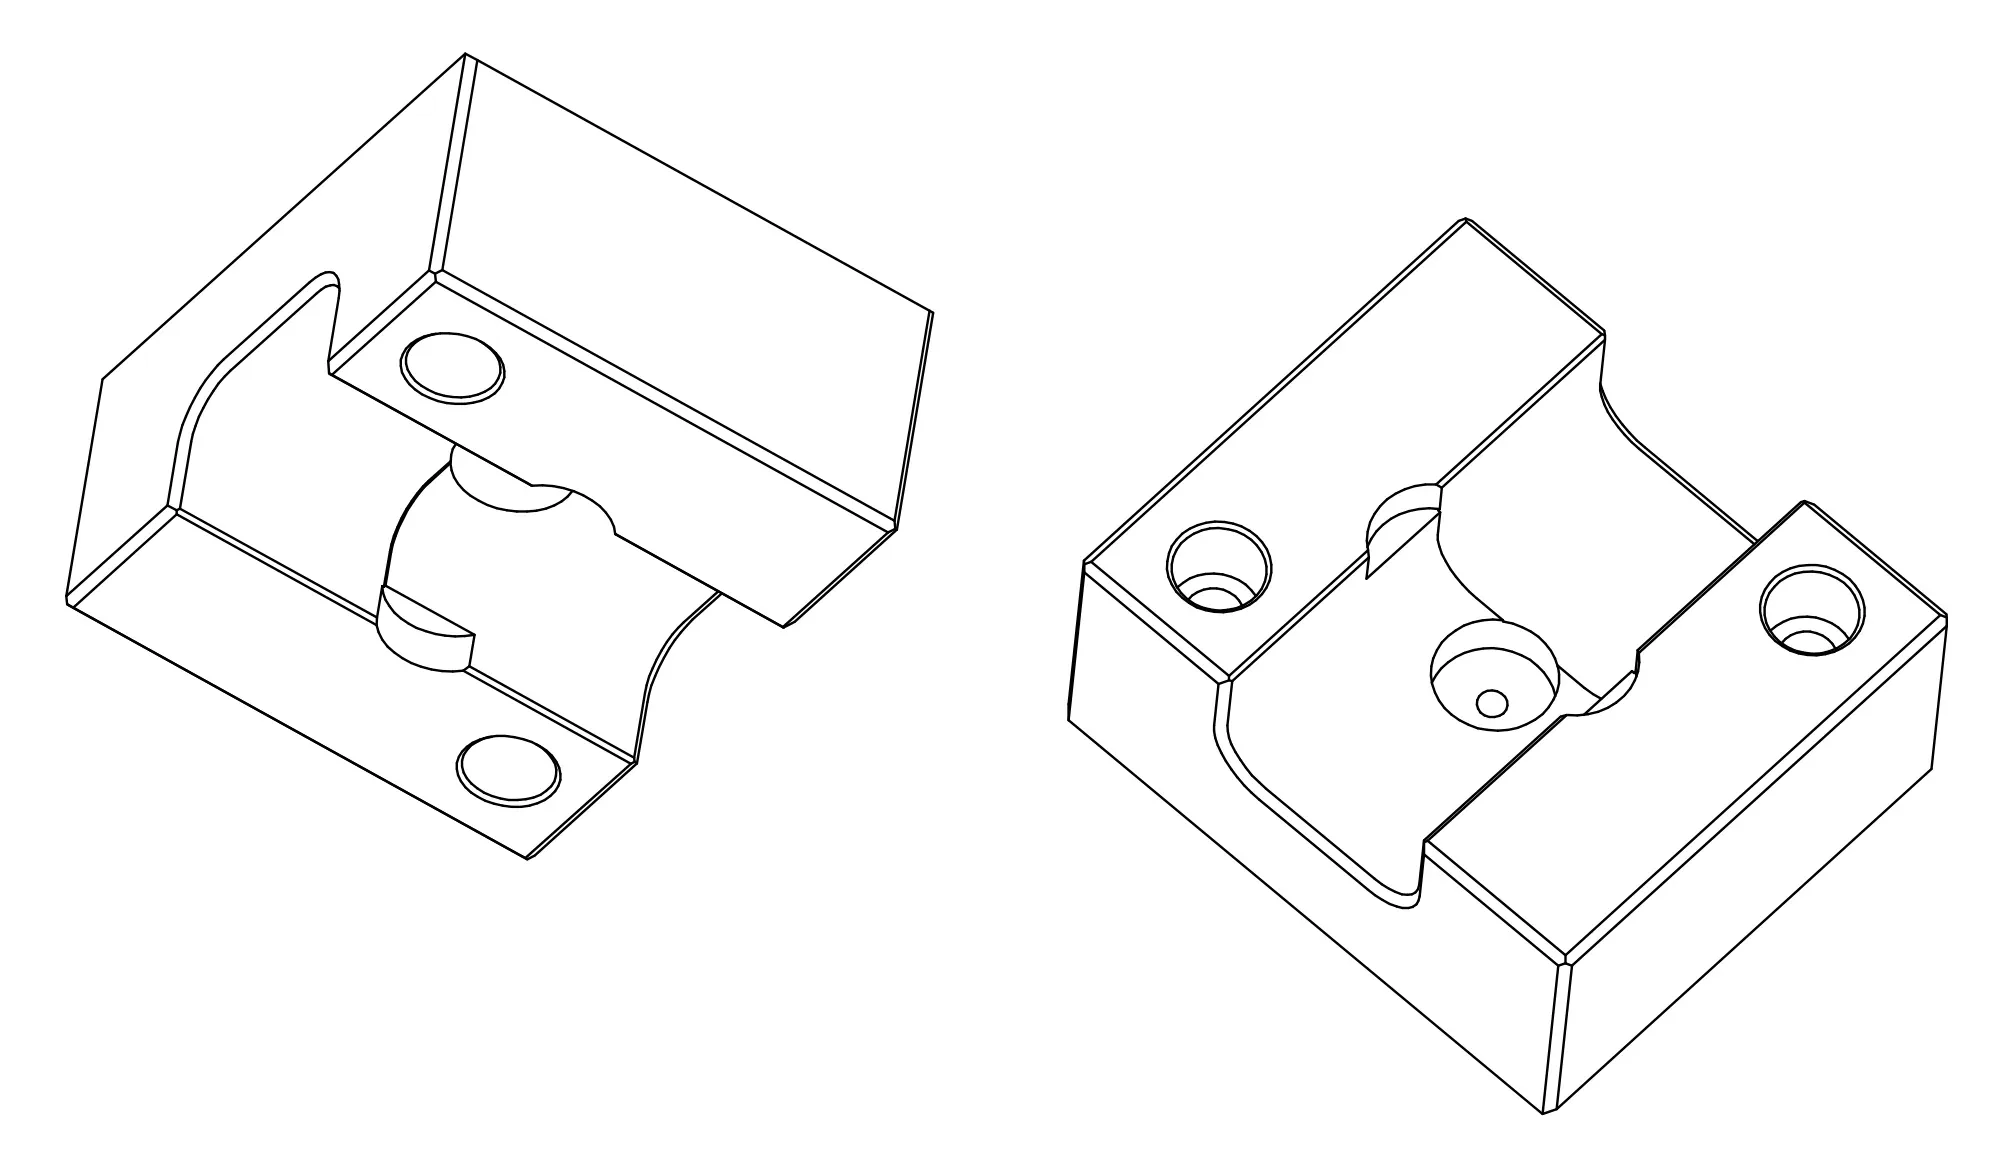
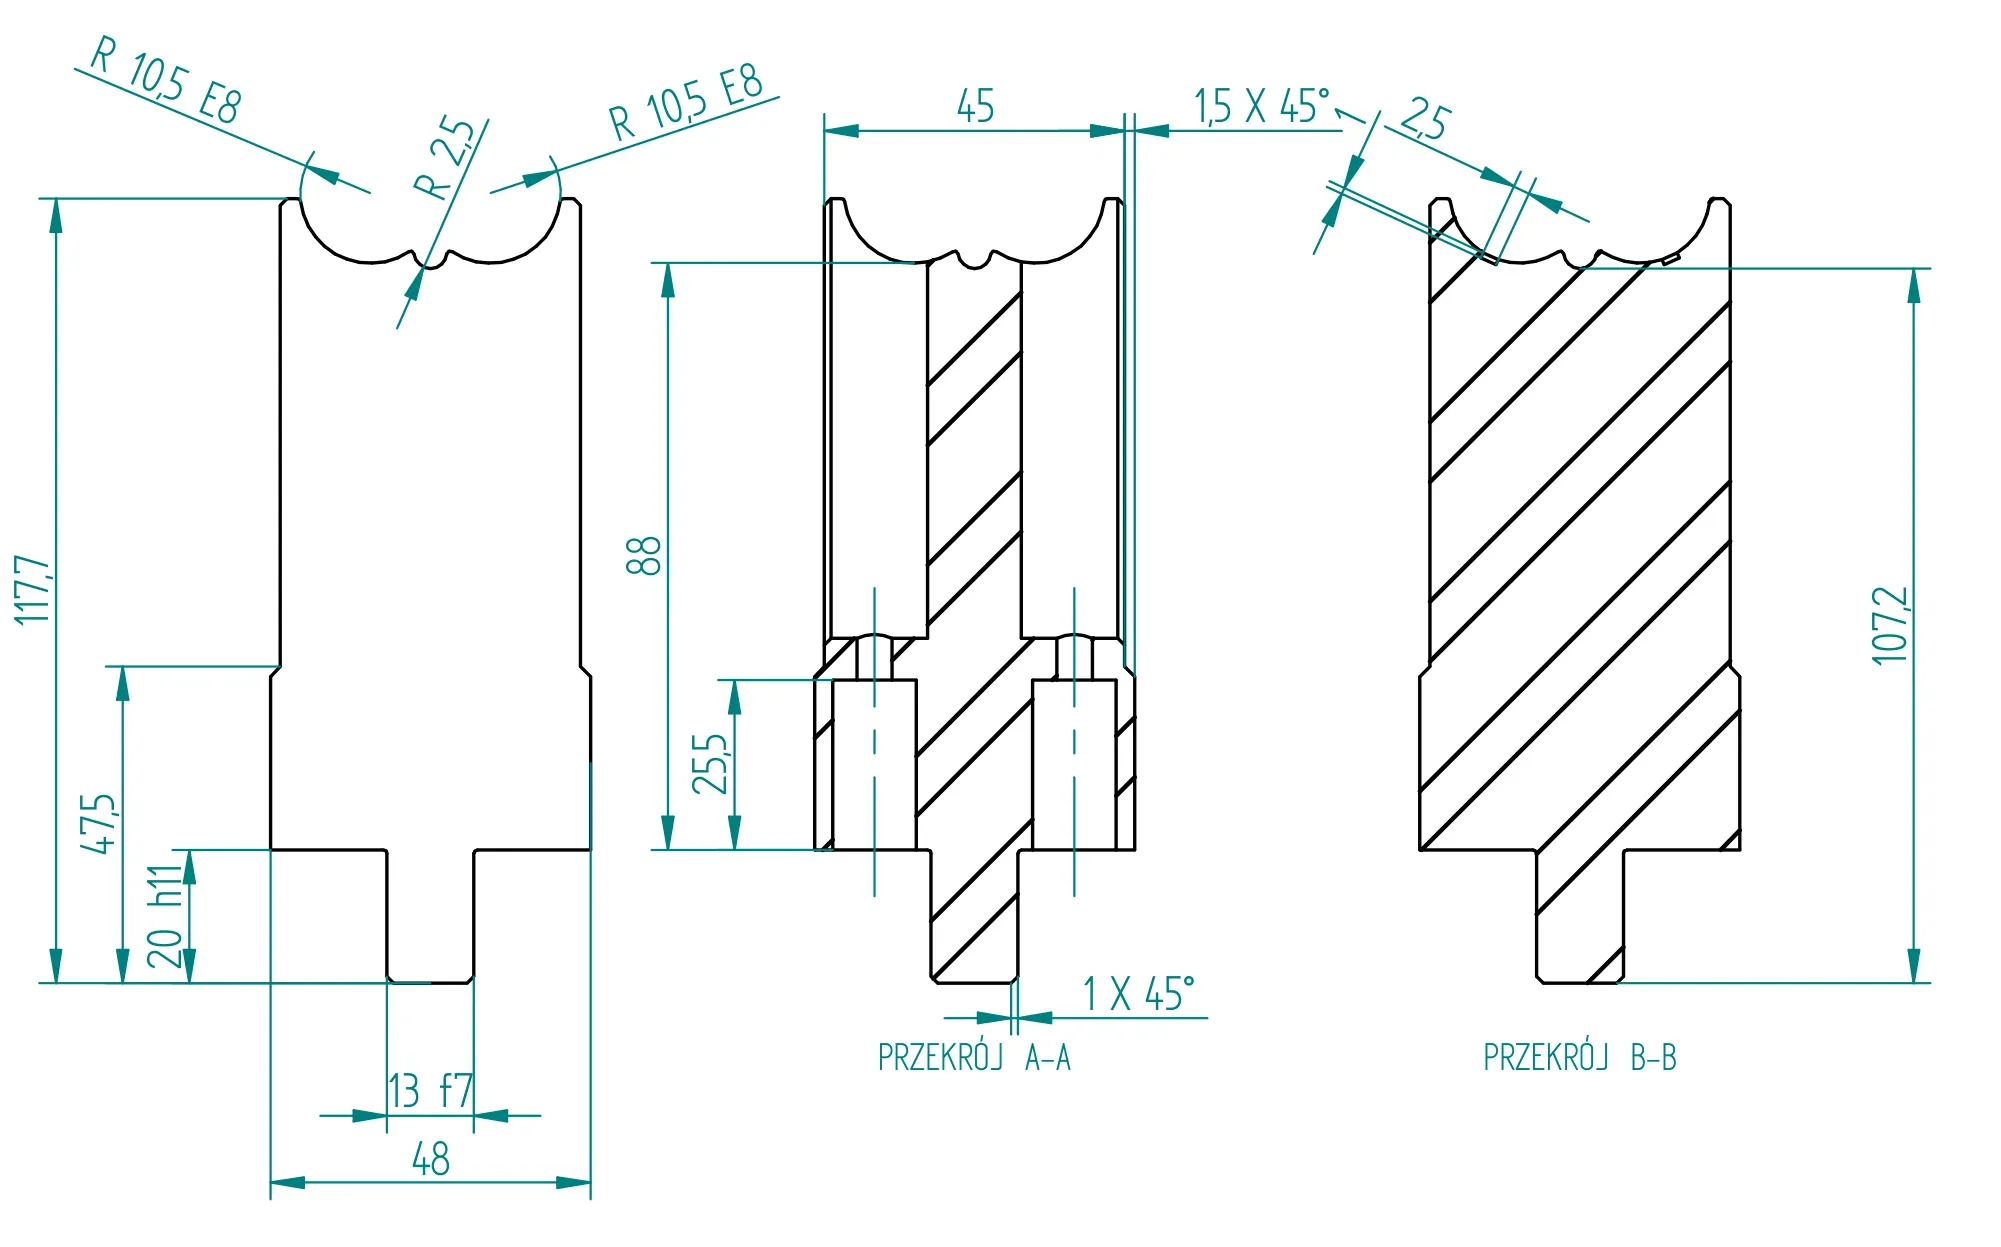
On our Mitsubishi FA20 wire EDM machine, we cut precision contours in electrically conductive materials, including hard and hardened grades (WEDM). The process is ideal for one-off parts and cutting tool profiles. We quote from a drawing or 3D model, from single pieces to series runs.
A thin wire removes material through electrical discharges.
Wire EDM (WEDM): wire cutting of hard and hardened materials
Wire electrical discharge machining (WEDM) is an electro-erosive machining process in which a thin wire removes material via electrical discharges rather than mechanical force. That is why wire EDM – also referred to as wire cutting or wire erosion – can cut hard and hardened materials alike. We cut contours on a Mitsubishi FA20 wire EDM machine based on a 2D drawing or 3D model.
Hard and hardened materials
Because there is no mechanical contact between the wire and the workpiece, post-hardening hardness does not limit cutting. The primary requirement is that the material be electrically conductive.
Contours for cutting tools
We use wire EDM to cut precision contours for cutting and forming tools, such as blanking dies and punches.
Precision parts
The method also excels at one-off, intricate geometries that are difficult to achieve by milling or turning.
- Wire EDM machine (WEDM)
- Mitsubishi
- Model
- FA20
- X/Y/Z axis travel
- 500 / 350 / 300 mm
- Max. workpiece weight
- 1,500 kg
- Wire diameter
- 0.1–0.3 mm
- Location
- ECAD, Lodz, Elektronowa 6
These are machine specifications, not finished part tolerances. We confirm tolerances when quoting.
Wire EDM of tool and hardened steels: blanking dies and punches
We manufacture blanking dies and punches from tool and hardened steels: the wire cuts their contours even after heat treatment. Example grades are listed below; the material must be electrically conductive. A broader overview of CNC materials can be found in the CNC machining materials table. Learn how we build complete tooling on our toolroom page.
| Material | Example grades |
|---|---|
| Cold-work tool steels (blanking dies, punches) | 1.2379 (X153CrMoV12, NC11LV, AISI D2) 1.2080 (X210Cr12, NC11, AISI D3) |
| Hardened and quenched & tempered steels | 42CrMo4 (1.7225, 40HM) C45 (1.0503) Hardox (wear-resistant steel) |
| Stainless and duplex steels | 1.4301 (AISI 304) 1.4404 (AISI 316L) duplex 1.4462 |
| Nickel alloys | Inconel 625, Inconel 718 |
- The grades in the table are examples and do not guarantee specific tolerances.
- Other electrically conductive materials, such as aluminium, copper or brass, are verified at the quoting stage.
- Workpiece height, contour geometry and tolerances are confirmed based on your drawing.
Wire EDM in the precision part production chain
We mill or turn the near-net shape of the workpiece and then use wire EDM to cut the precision contour, including in pre-hardened material. Reference datum surfaces are ground prior to wire cutting, and finished part dimensions can be verified with a 3D scanner. See the full range of services under CNC machining.
CNC milling or turning
Roughing and pre-machining of the workpiece on CNC machining centres or lathes.
Surface grinding
We grind datum surfaces for wire cutting on our Okamoto surface grinder.
Wire EDM
We cut precise contours by wire on our Mitsubishi FA20 wire EDM machine, including in hard or hardened materials.
3D inspection
We can check the dimensions of the finished part using a 3D scanner and a Mitutoyo height gauge.
What to send for a wire EDM quote
We quote wire EDM based on a drawing or 3D model, not from a price list. We accept orders from single parts to series runs.
Send a drawing or 3D model
PDF, DXF, DWG, STEP, IGES, photos (JPG, PNG, TIFF) or a ZIP or 7Z archive. Up to 10 files, up to 100 MB in total.
Describe your order
Material, part thickness or height, quantity and lead time.
We will reply with any questions and a price
We will check whether the material is suitable for wire EDM and send you a quote.
The order price will depend on:
- the material and its electrical conductivity
- part thickness or height (Z-axis travel 300 mm)
- contour complexity and number of openings
- quantity
- lead time
Prefer to call? +48 697 270 000 (Mon–Fri 8:00–16:00)
Prefer e-mail? biuro@ecad.com.pl
We process enquiry data in accordance with our privacy policy.
Questions about wire EDM
What is wire EDM (WEDM)?
It is an electrical discharge machining method: a thin wire removes material using electrical discharges, without mechanical pressure. Wire EDM is also known as wire cutting or wire erosion. We cut the contour on a Mitsubishi FA20 wire EDM machine from a drawing or 3D model.
How does the wire EDM process work?
A thin wire with a diameter of 0.1–0.3 mm passes right through the workpiece. Electrical discharges jump between the wire and the material, removing material along a contour programmed from a drawing or 3D model. Because the wire does not touch the workpiece, wire cutting produces a precise contour even in hardened steel. We grind the datum surfaces beforehand on our Okamoto grinder and cut the contour on our Mitsubishi FA20 wire EDM machine.
Can you cut hardened or very hard steel?
Yes. The wire does not make mechanical contact with the part, so material hardness after hardening is not an obstacle. The primary requirement is that the material is electrically conductive.
Which materials are suitable for wire EDM?
Electrically conductive materials: tool and hardened steels (which we use to make blanking dies and punches, among other tools), stainless steels, nickel alloys, and other metals and alloys. Example grades are listed in the material table. When preparing your quote, we will verify whether your material is suitable.
How does wire EDM differ from sinker EDM?
Wire EDM cuts a contour right through the material using a thin wire, whereas sinker EDM erodes a blind cavity in a solid block using an electrode shaped as the inverse of the cavity. Both methods are electrical discharge machining processes. At ECAD, we operate a Mitsubishi FA20 wire EDM machine and use it to perform wire EDM.
How large a part can you cut on the Mitsubishi FA20 wire EDM machine?
We cut contours within an X/Y axis travel range of 500 × 350 mm, with a Z-axis travel of 300 mm and a workpiece weight of up to 1,500 kg. These are the machine parameters. When quoting based on your drawing, we confirm whether your part will fit and what contour we can achieve.
What is wire EDM used for?
Wire EDM is used for precise contours in hard and hardened materials, including in cutting and forming tools, wherever a contour is difficult to achieve by milling or turning.
How much does wire EDM cost?
We quote based on a drawing or 3D model, not from a price list. The price depends on the material, part thickness or height, contour complexity, quantity and lead time. We accept orders from a single part.
Wire EDM in Lodz, Elektronowa 6
The Mitsubishi FA20 wire EDM machine operates at our plant at ul. Elektronowa 6 in Lodz, open Monday to Friday from 8:00 to 16:00. We have been operating since 2008 and employ 25 people. We hold an ISO 9001:2015 certificate for the forming and machining of metal components as well as machine design and building. See also the Mitsubishi FA20 in our machine park, contact and directions, and our full service range.
Have a precise contour to cut?
Send a drawing or 3D model. We will check whether the material is suitable for wire EDM and quote your order, from a single part to a series run.


