Sheet metal bending
in Lodz
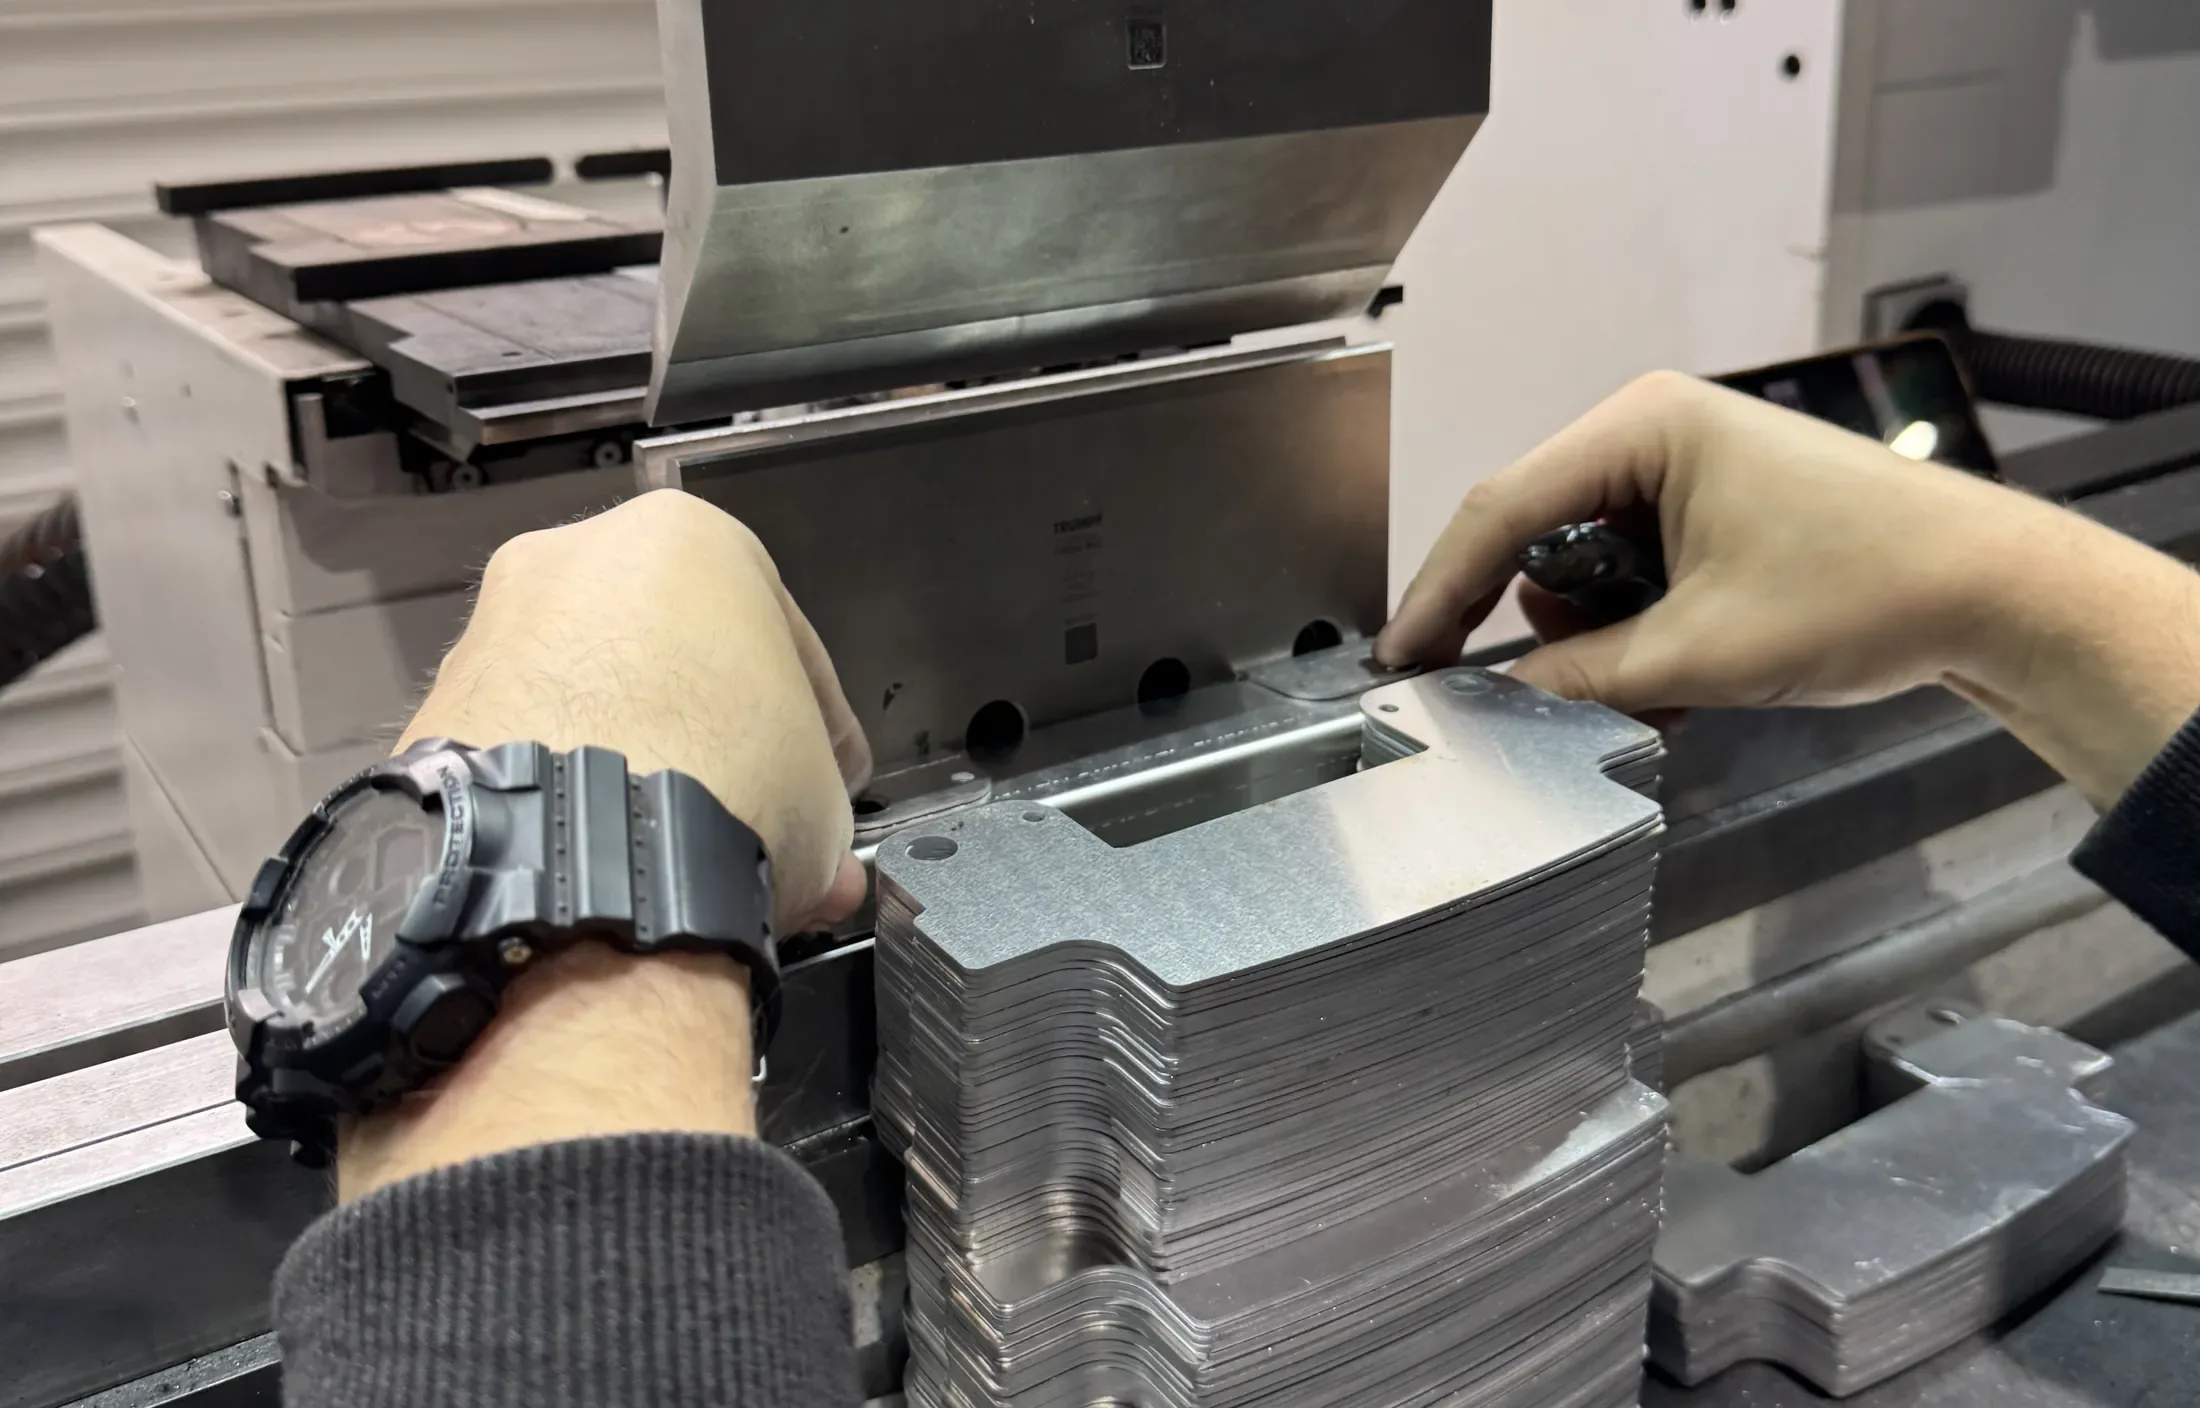
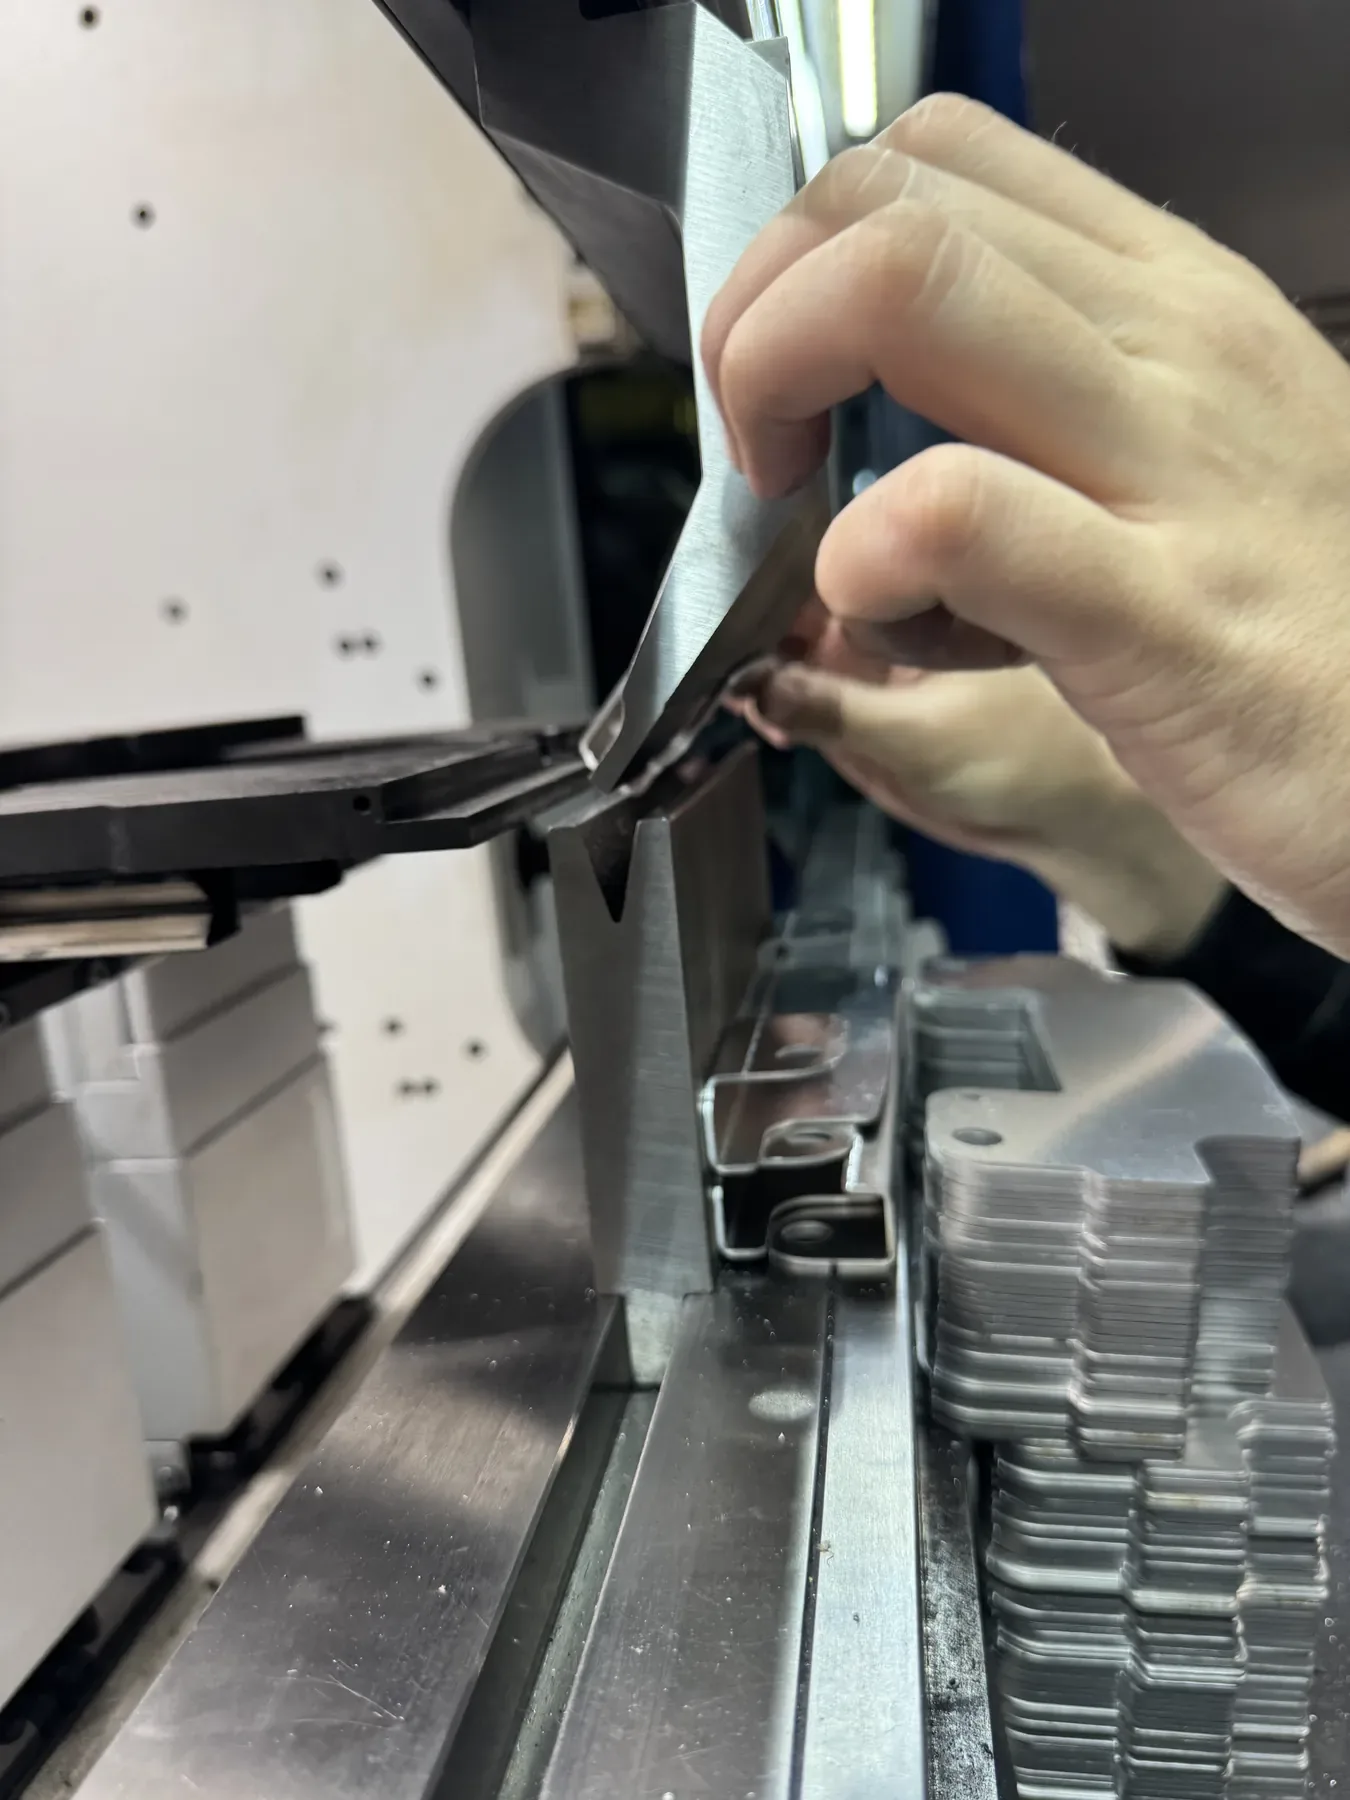
Blank in the tooling of a Trumpf press brake. ECAD shop floor.
- Pressing force
- 500 kN
- Bending length
- 1530 mm
- Backgauge
- 6 axes
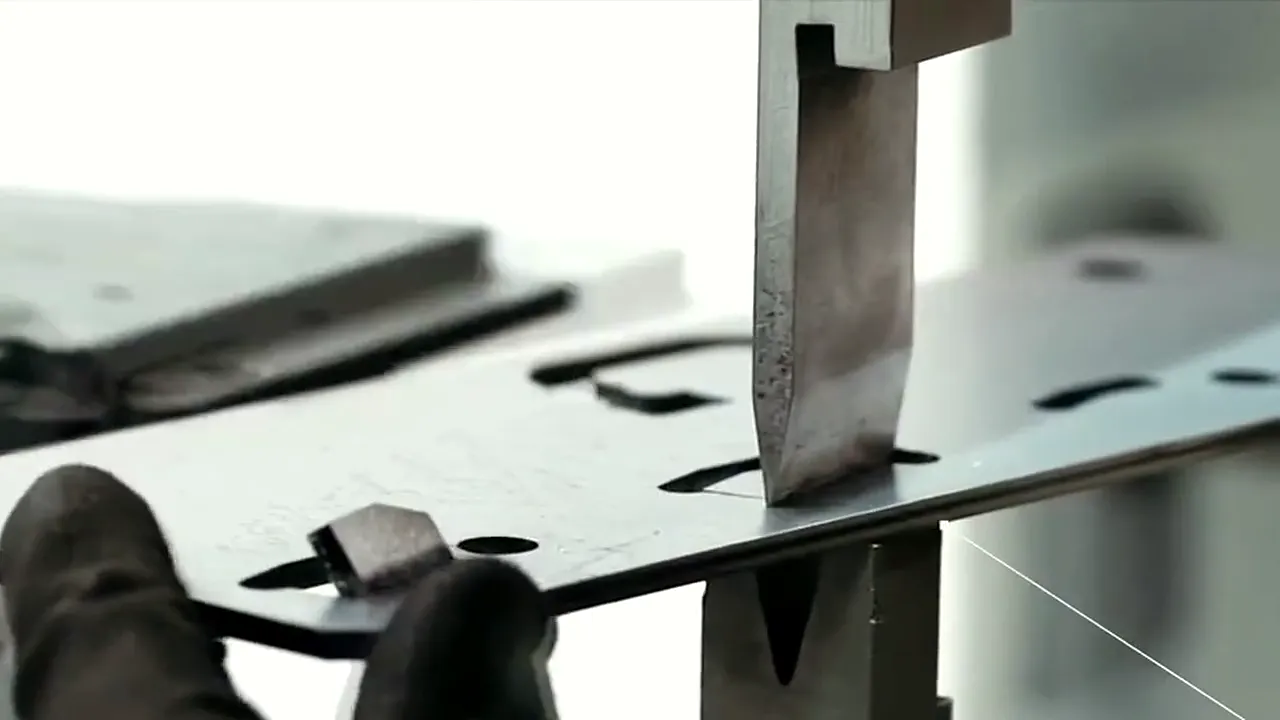
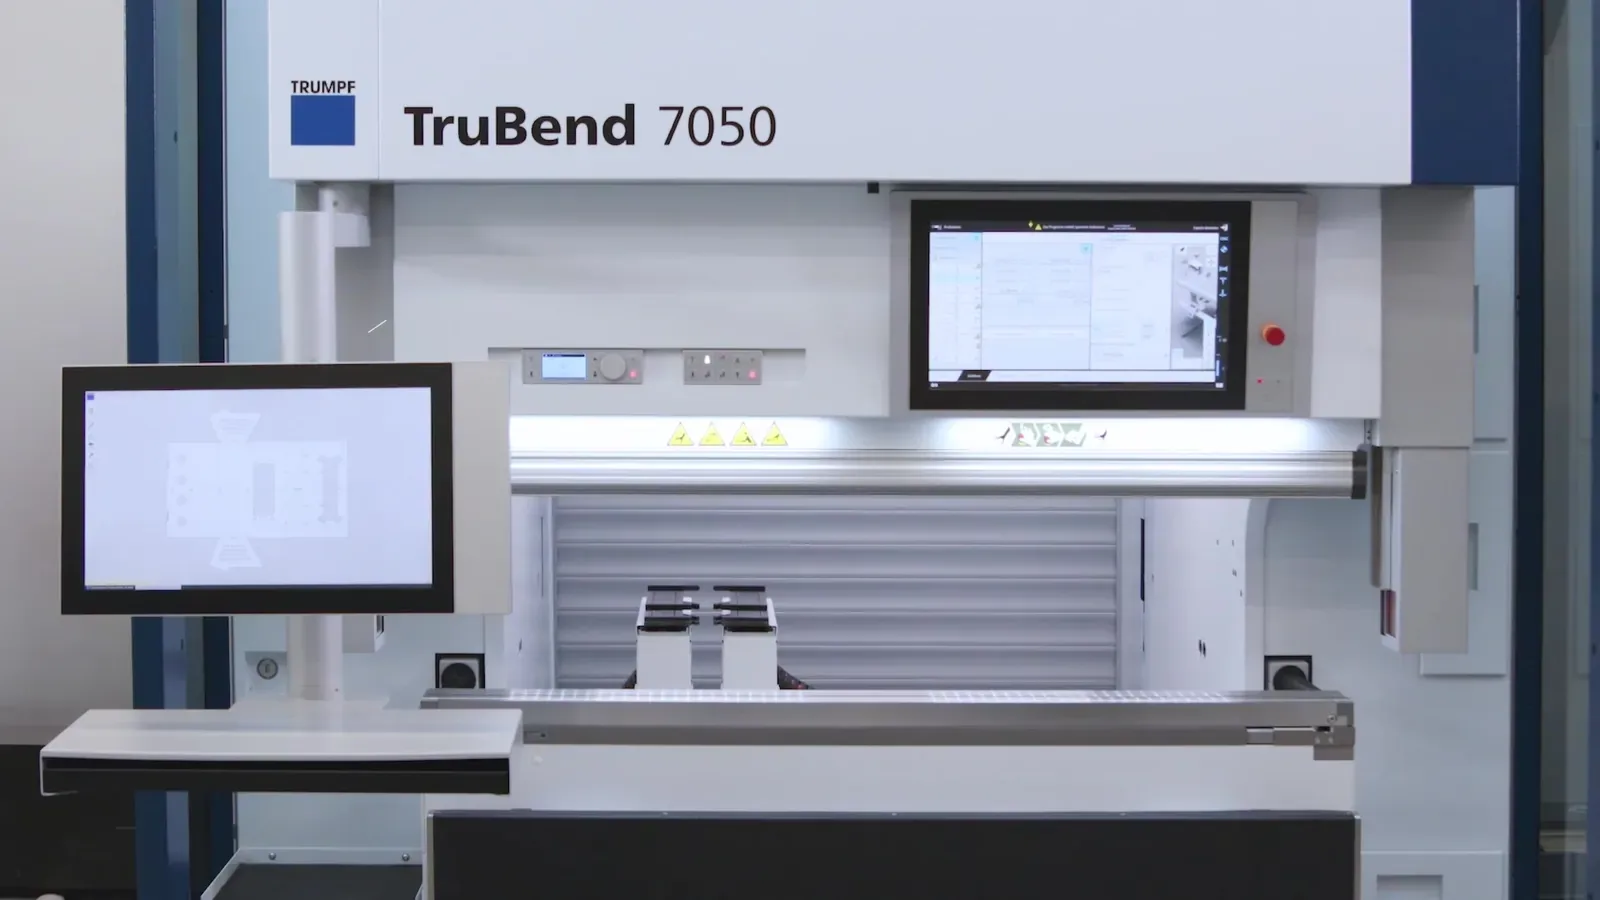
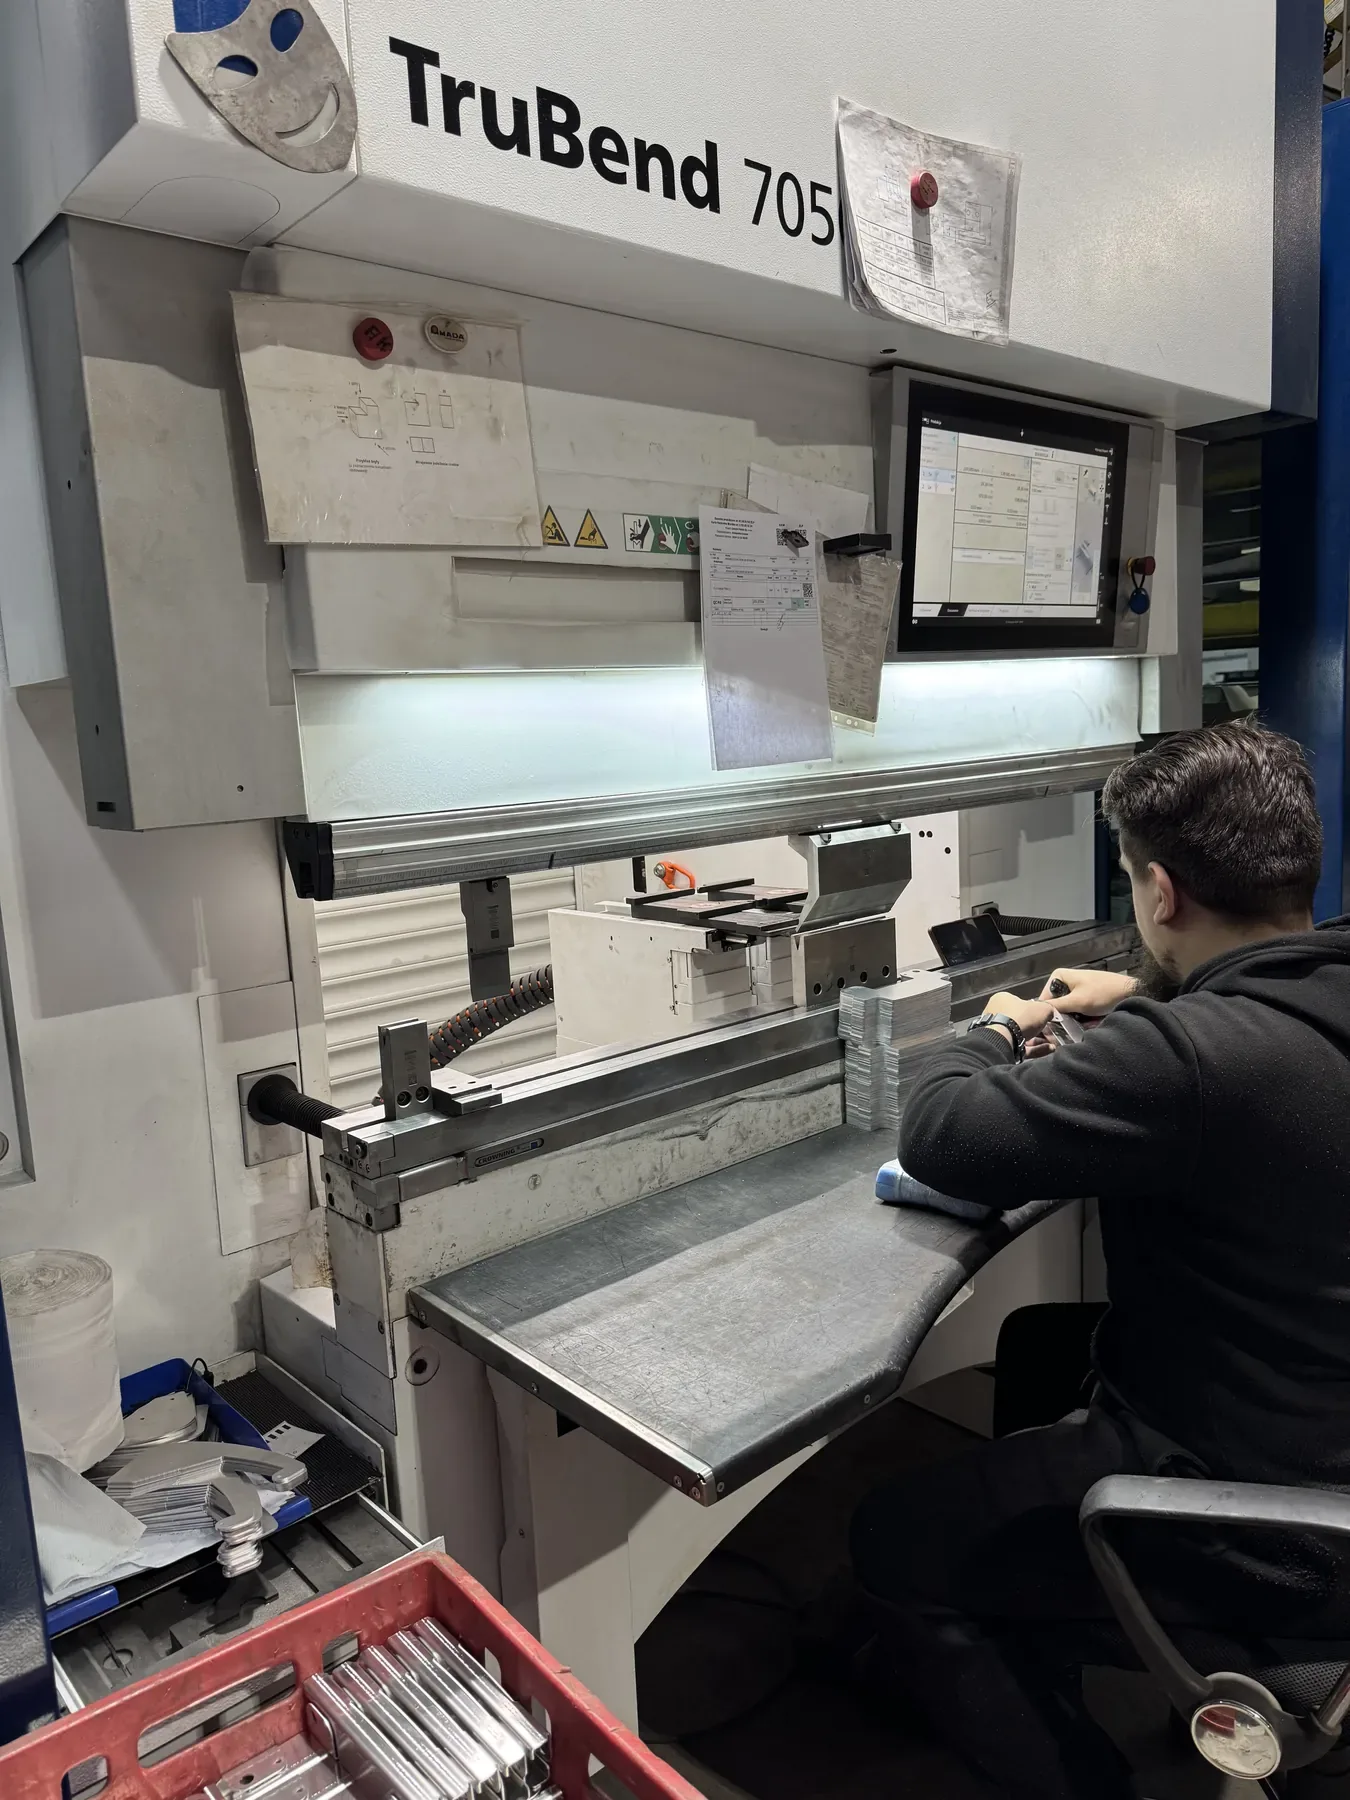
Custom sheet metal bending on our Trumpf TruBend 7050 press brake: from a drawing or 3D model, from one-offs to series production. We prepare the bending programme in SigmaBEND. We cut the sheet metal on our 12 kW laser, deburr and bend it in a single order.
Custom sheet metal bending on a Trumpf TruBend 7050 press brake
CNC bending on the TruBend 7050 is fast: the press brake handles small and medium-sized parts well, including series orders. A second press brake, the Trumpf TruBend 3130 (planned for November 2026), with a longer beam for larger parts, will join our fleet soon.
| Parameter | TruBend 7050 | TruBend 3130, coming soon |
|---|---|---|
| Pressing force | 500 kN | 1300 kN |
| Bending length | 1530 mm | 3230 mm |
| Open height | 385 mm | 615 mm |
| Backgauge | 6 axes | 4 axes |
| Safety | – | BendGuard |
| Status | in operation | coming soon, planned for November 2026 |
The maximum bending thickness depends on the pressing force, bending length, material and die width. This is shown in the bending table below.
Sheet metal bending table: die, punch and pressing force
Approximate 90° air bending force for structural steel (Rm ≈ 450 MPa), in tonnes per metre of bending length. The orange cells show the recommended die opening (V ≈ 8 × sheet thickness). Values are calculated using the air bending force formula and compared against TRUMPF and AMADA force charts.
Scroll the table sideways.
| V-die [mm] | 6 | 8 | 10 | 12 | 16 | 20 | 25 | 32 | 40 | 50 | 63 | 80 | 100 | Max. bending length on TruBend 7050 |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Inside radius ri [mm] | 1 | 1.3 | 1.6 | 2 | 2.6 | 3.3 | 4 | 5 | 6.5 | 8 | 10 | 13 | 16 | |
| Min. flange b [mm] | 4 | 5.5 | 7 | 8.5 | 11 | 14 | 17.5 | 22 | 28 | 35 | 45 | 55 | 71 | |
| 0.5 mm | 2.5 | full length (1530 mm) | ||||||||||||
| 0.8 mm | 7 | 5 | 4 | full length (1530 mm) | ||||||||||
| 1 mm | 11* | 8* | 6.5 | 5.5* | full length (1530 mm) | |||||||||
| 1.5 mm | 18* | 15 | 12 | 9 | 7.5 | full length (1530 mm) | ||||||||
| 2 mm | 26 | 22 | 16 | 13 | 10 | full length (1530 mm) | ||||||||
| 2.5 mm | 25 | 20 | 16 | 13 | full length (1530 mm) | |||||||||
| 3 mm | 37 | 29 | 23 | 18 | 15 | full length (1530 mm) | ||||||||
| 4 mm | 52 | 42 | 33 | 26 | 21 | full length (1530 mm) | ||||||||
| 5 mm | 65 | 51 | 41 | 33 | 26 | up to 1250 mm | ||||||||
| 6 mm | 73 | 59 | 47 | 37 | 29 | up to 1080 mm | ||||||||
| 8 mm | 104 | 83 | 66 | 52 | 42 | up to 770 mm | ||||||||
| 10 mm | 130 | 103 | 81 | 65 | up to 620 mm | |||||||||
| 12 mm | 149 | 117 | 94 | up to 540 mm |
- recommended die for the given thickness
- over 33 t/m: shorter bends only on the TruBend 7050 (last column)
- * manufacturers’ tables state up to 30% higher force here for thin sheet metal in a narrow die
Punch and die
Up to approx. 3 mm, a punch 86–88° with an R0.6–R1 tip is normally used; for thicker sheet metal: R3–R4 tip. The die opening is selected at 6–12 × sheet thickness; a wider die means lower force and a larger bend radius.
Bending aluminium, stainless steel and other materials
The force from the table is multiplied by the tensile strength ratio: for stainless steel (e.g. 1.4301) approx. × 1.5, for aluminium (e.g. 5754) approx. × 0.5, and for DC01 steel approx. × 0.6–0.9. Bending aluminium therefore requires less force than bending structural steel, while stainless steel requires more.
What this means for your part
Over the full length of 1530 mm, the TruBend 7050 bends structural steel up to approx. 4 mm, and thicker sheet metal over shorter lengths. We confirm the bending tools and force for your specific part when preparing the quote.
Indicative values for 90° air bending, calculated using the formula P = 1.42 × Rm × s² / V and compared with TRUMPF and AMADA force tables; inside radius and minimum flange according to the AMADA tool catalogue, punch selection according to TRUMPF and AMADA catalogues. The actual tensile strength of S235 sheet metal is 360–510 MPa, so the required force may vary by a dozen or so percent.
From flat pattern to finished guard
Flat pattern from our design (Solid Edge)
Our design office designed this transport guard in Solid Edge. The 3D model generates a DXF flat pattern: 5 mm steel, 435 × 353 mm blank, outer contour and 17 holes.
Bending programme in SigmaBEND
We prepare bending programmes in SigmaBEND. The drawing for this guard includes a bending table: four 90° bends, 5.8 mm inside radius, plus the sequence and direction of each bend.

Bending simulation in SigmaBEND (different part) Bending on the Trumpf TruBend 7050 press brake
We bend the part on our Trumpf TruBend 7050 press brake (500 kN, bending length up to 1530 mm). Sequence from the drawing: flange with slotted holes, wall with Ø40 holes, then left and right lugs.
Finished guard
After four bends, the guard measures 435 × 224 × 145 mm. We laser cut, deburr and bend in a single order. See bent sheet metal assemblies in our projects.
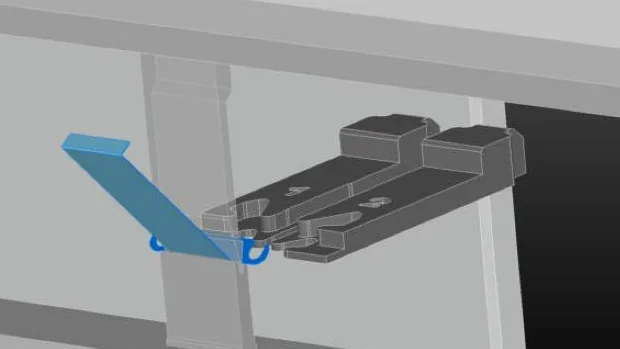
Laser cutting and sheet metal bending in one order, including deburring
We cut blanks for bending in-house on our 12 kW laser: you do not need to order laser cutting from another supplier. After bending, we can weld the parts into a finished assembly. See welded structures and full-service production.
Laser-cut blank
12 kW fibre laser, 3000 × 1500 mm sheets.
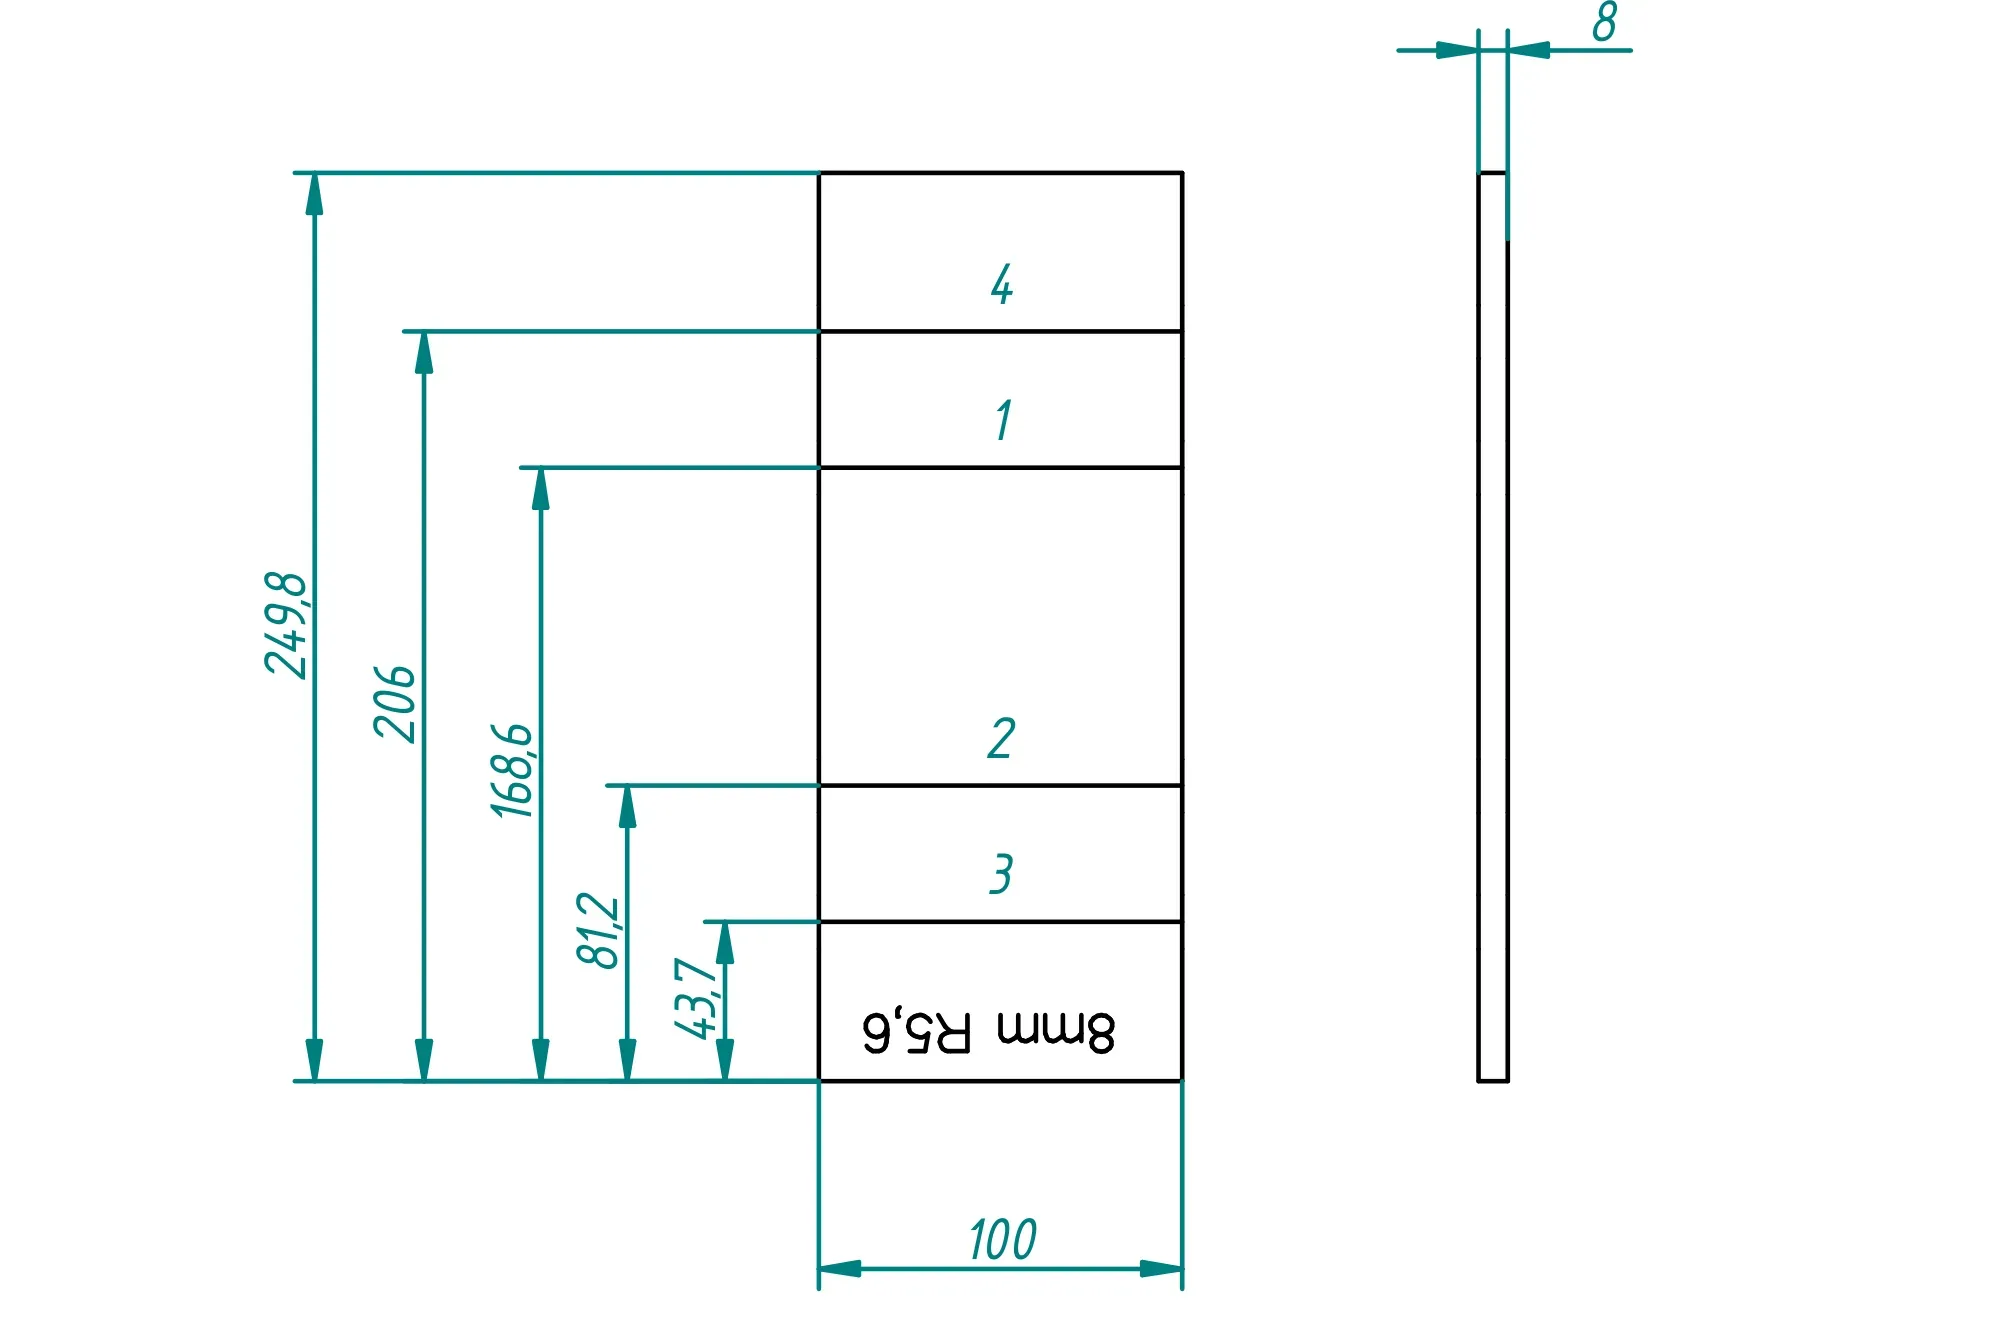
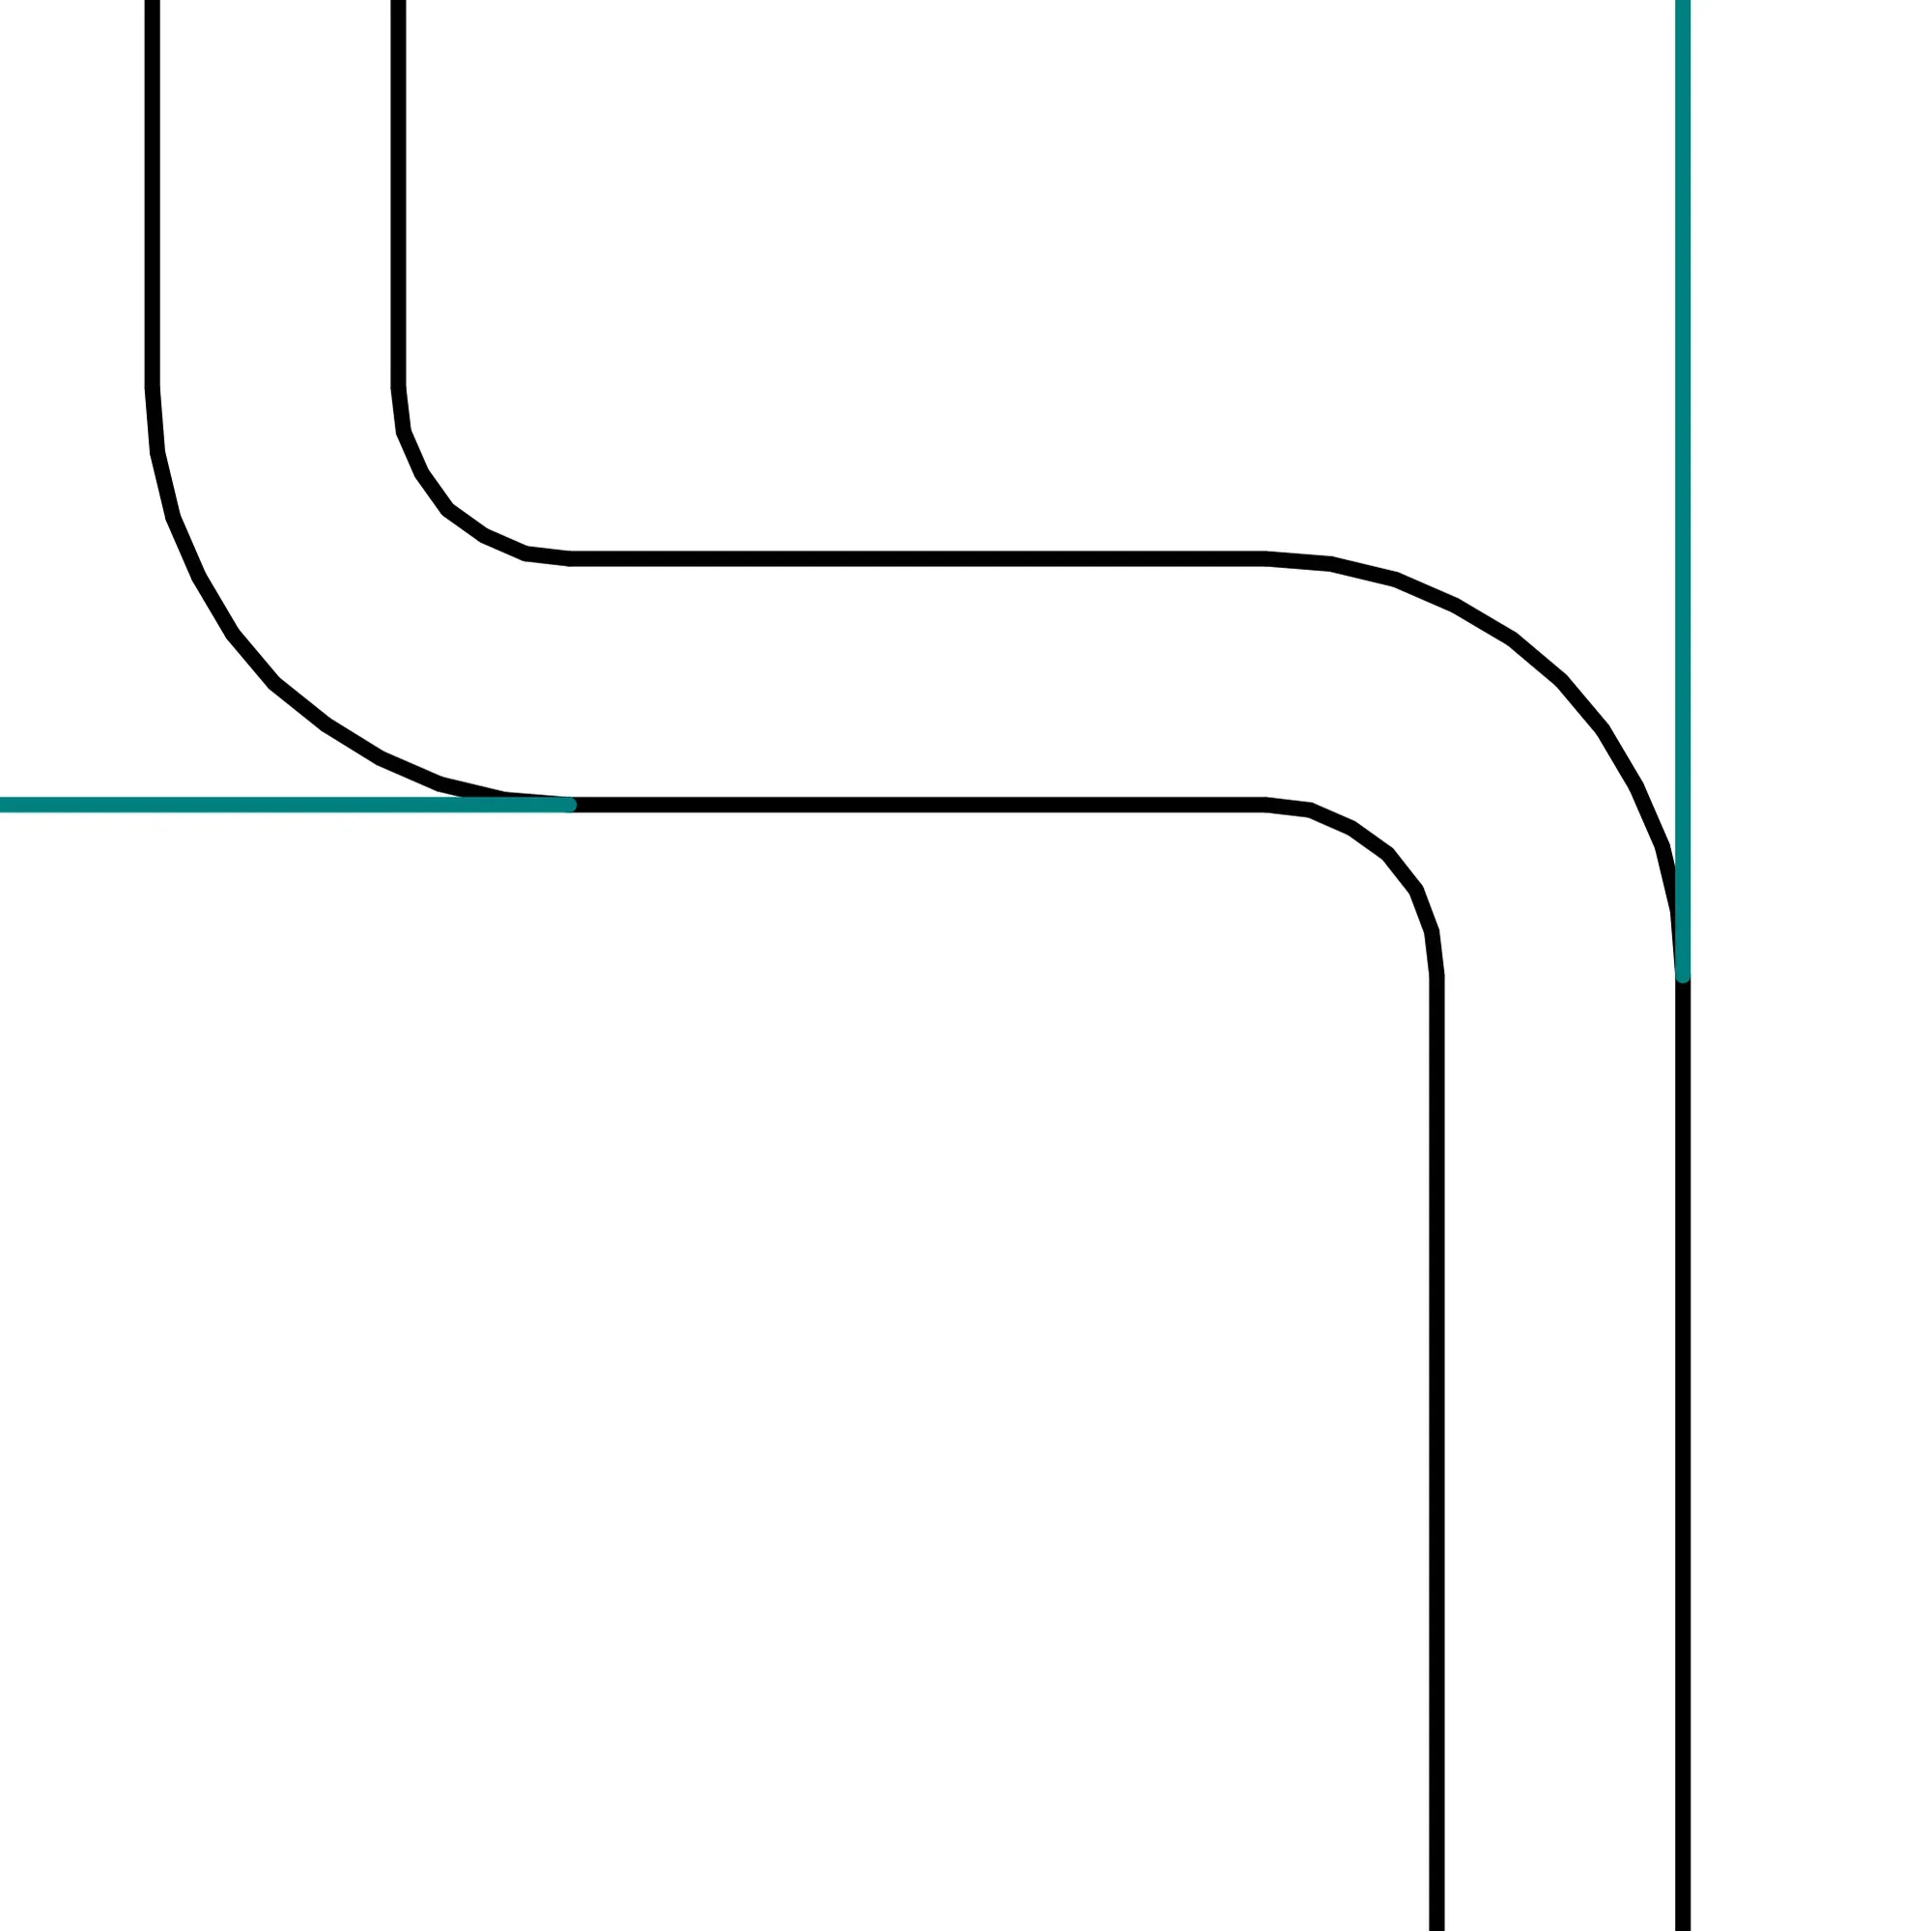
Sheet metal flat pattern: numbers indicate the bending sequence. Drawing from the ECAD archive.
Sheet metal laser cuttingDeburring
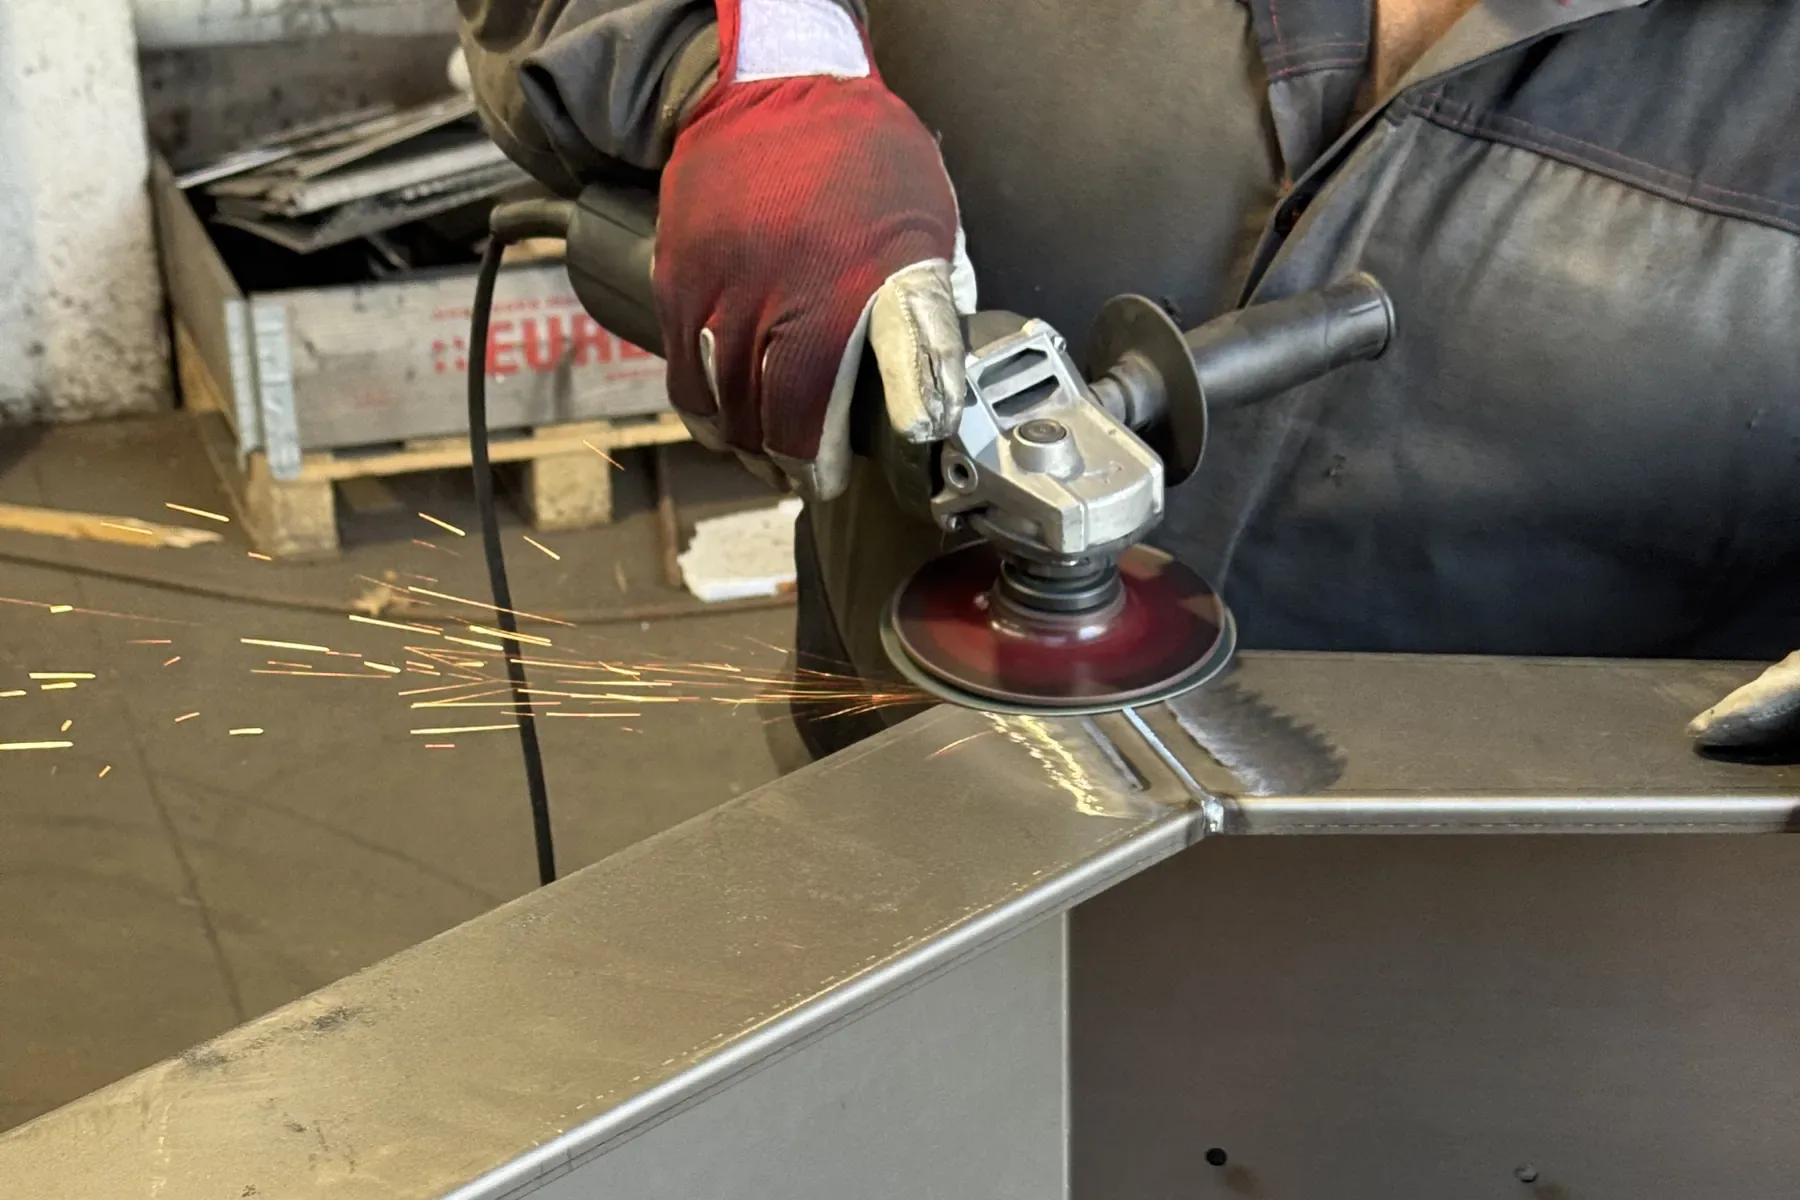
We remove burrs from edges after cutting.
Angle grinder at the corner of a bent sheet metal part. ECAD shop floor.
Sheet metal bending
Trumpf TruBend 7050 press brake, from one-off parts to series production.
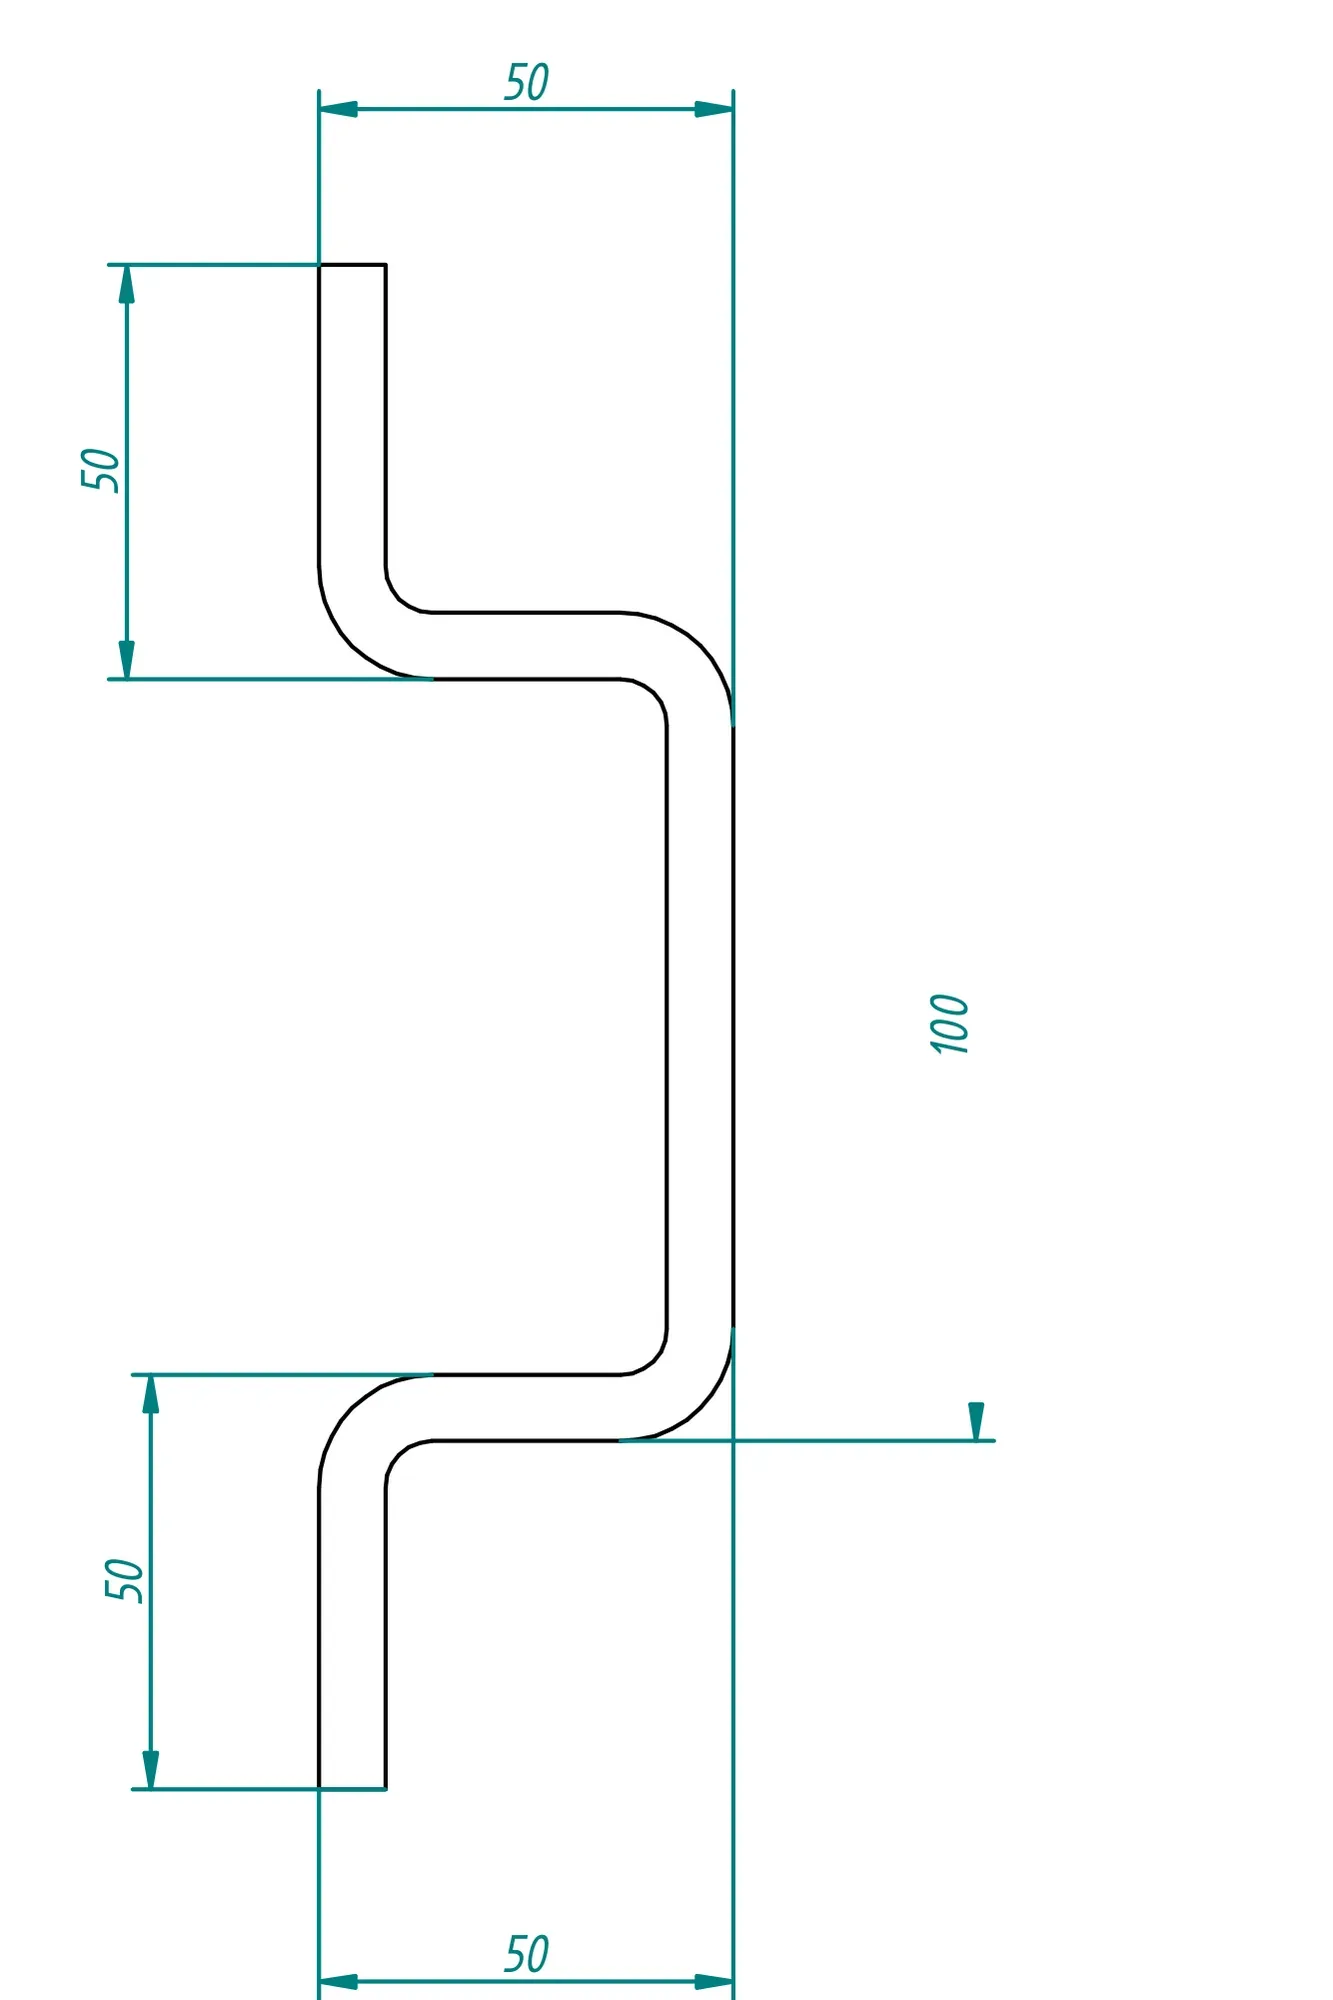
Profile after four bends, with dimensions. Close-up of the bends: inside and outside bend radius.
Welding
Manual and robotic welding, including welding for the rail industry to EN 15085-2.
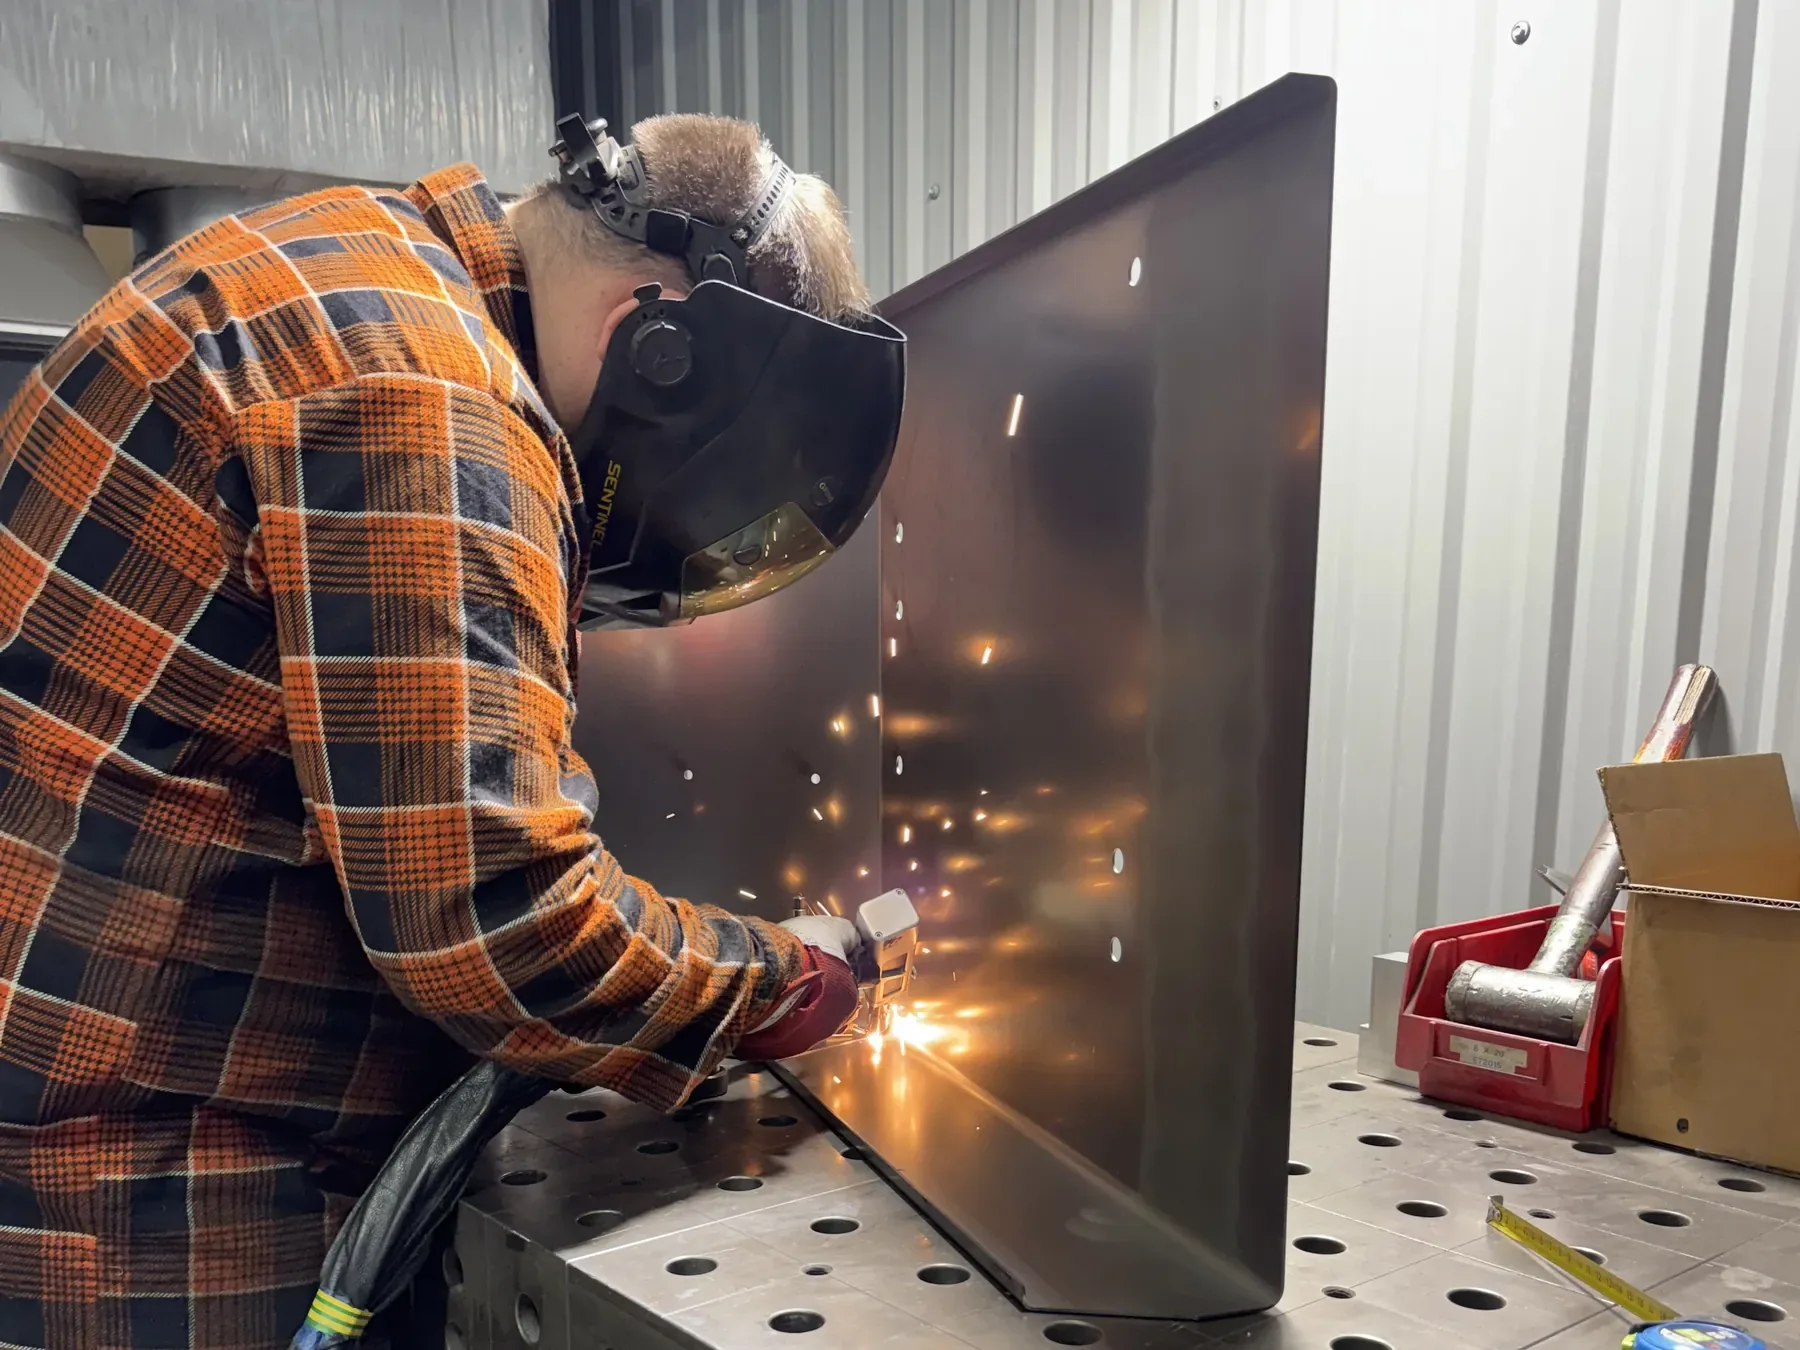
Welding a sheet metal part on a perforated welding table. ECAD shop floor.
Welding
Sheet metal bending in Lodz, ul. Elektronowa 6
We perform sheet metal bending in Lodz at our plant at ul. Elektronowa 6, open Monday to Friday from 8:00 to 16:00. We have been operating since 2008 and employ 25 people. See contact and directions and our machine park.
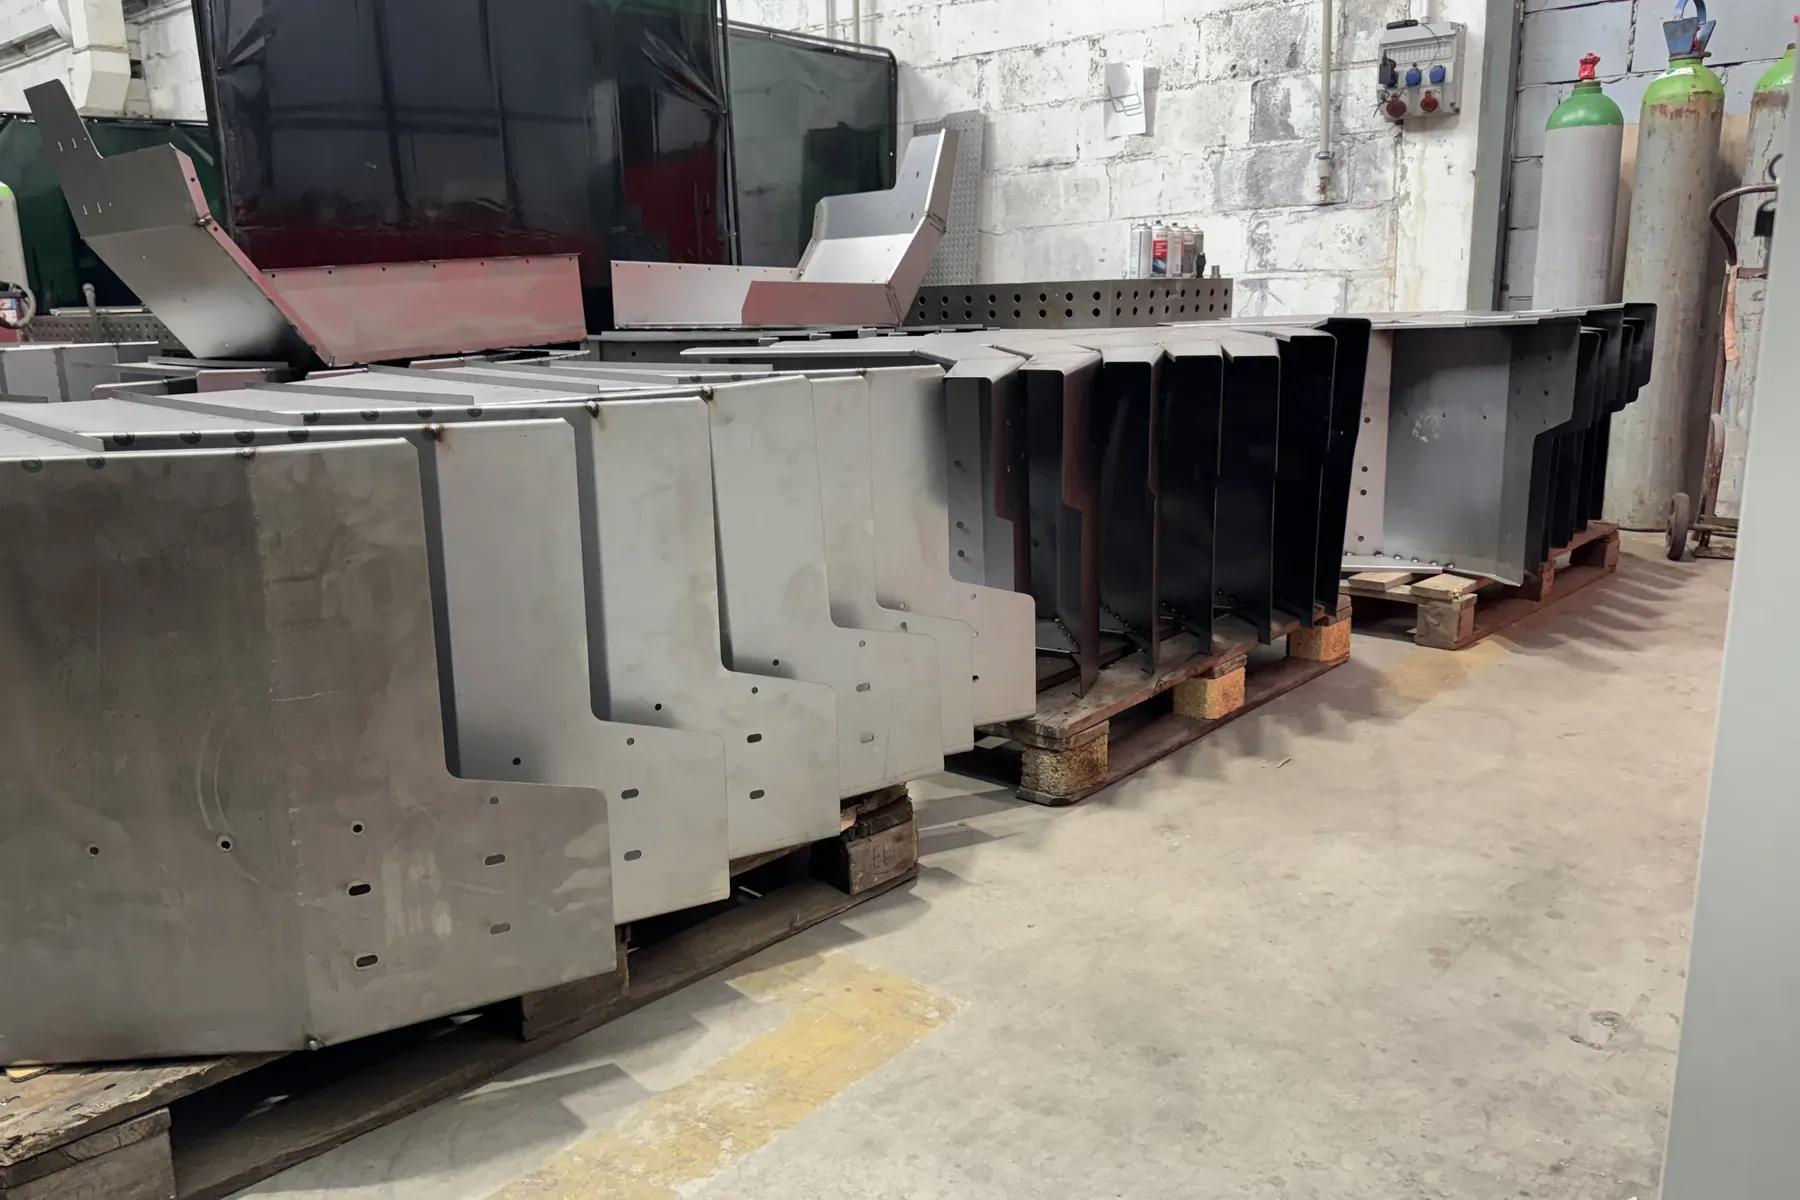
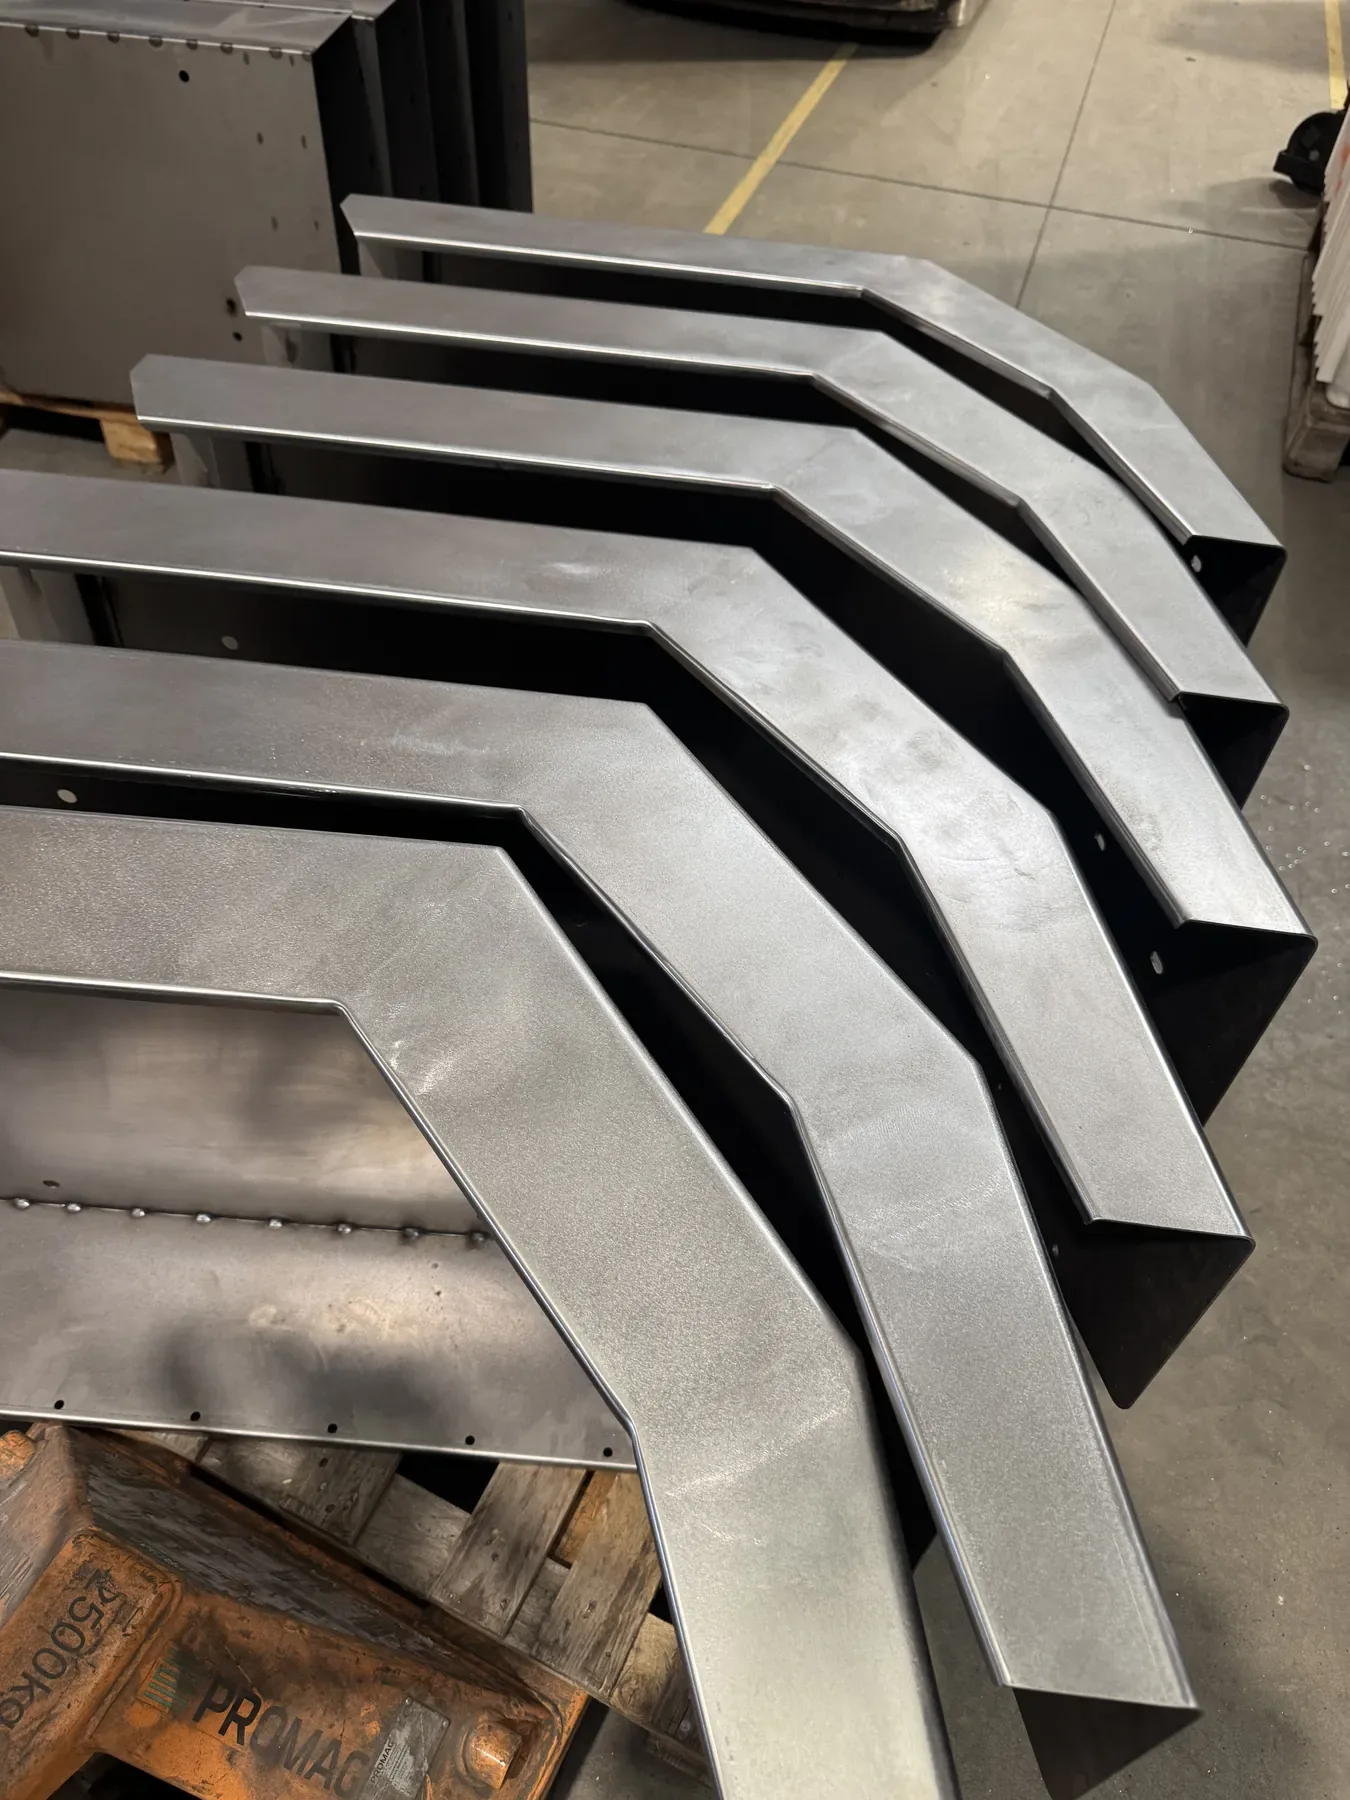
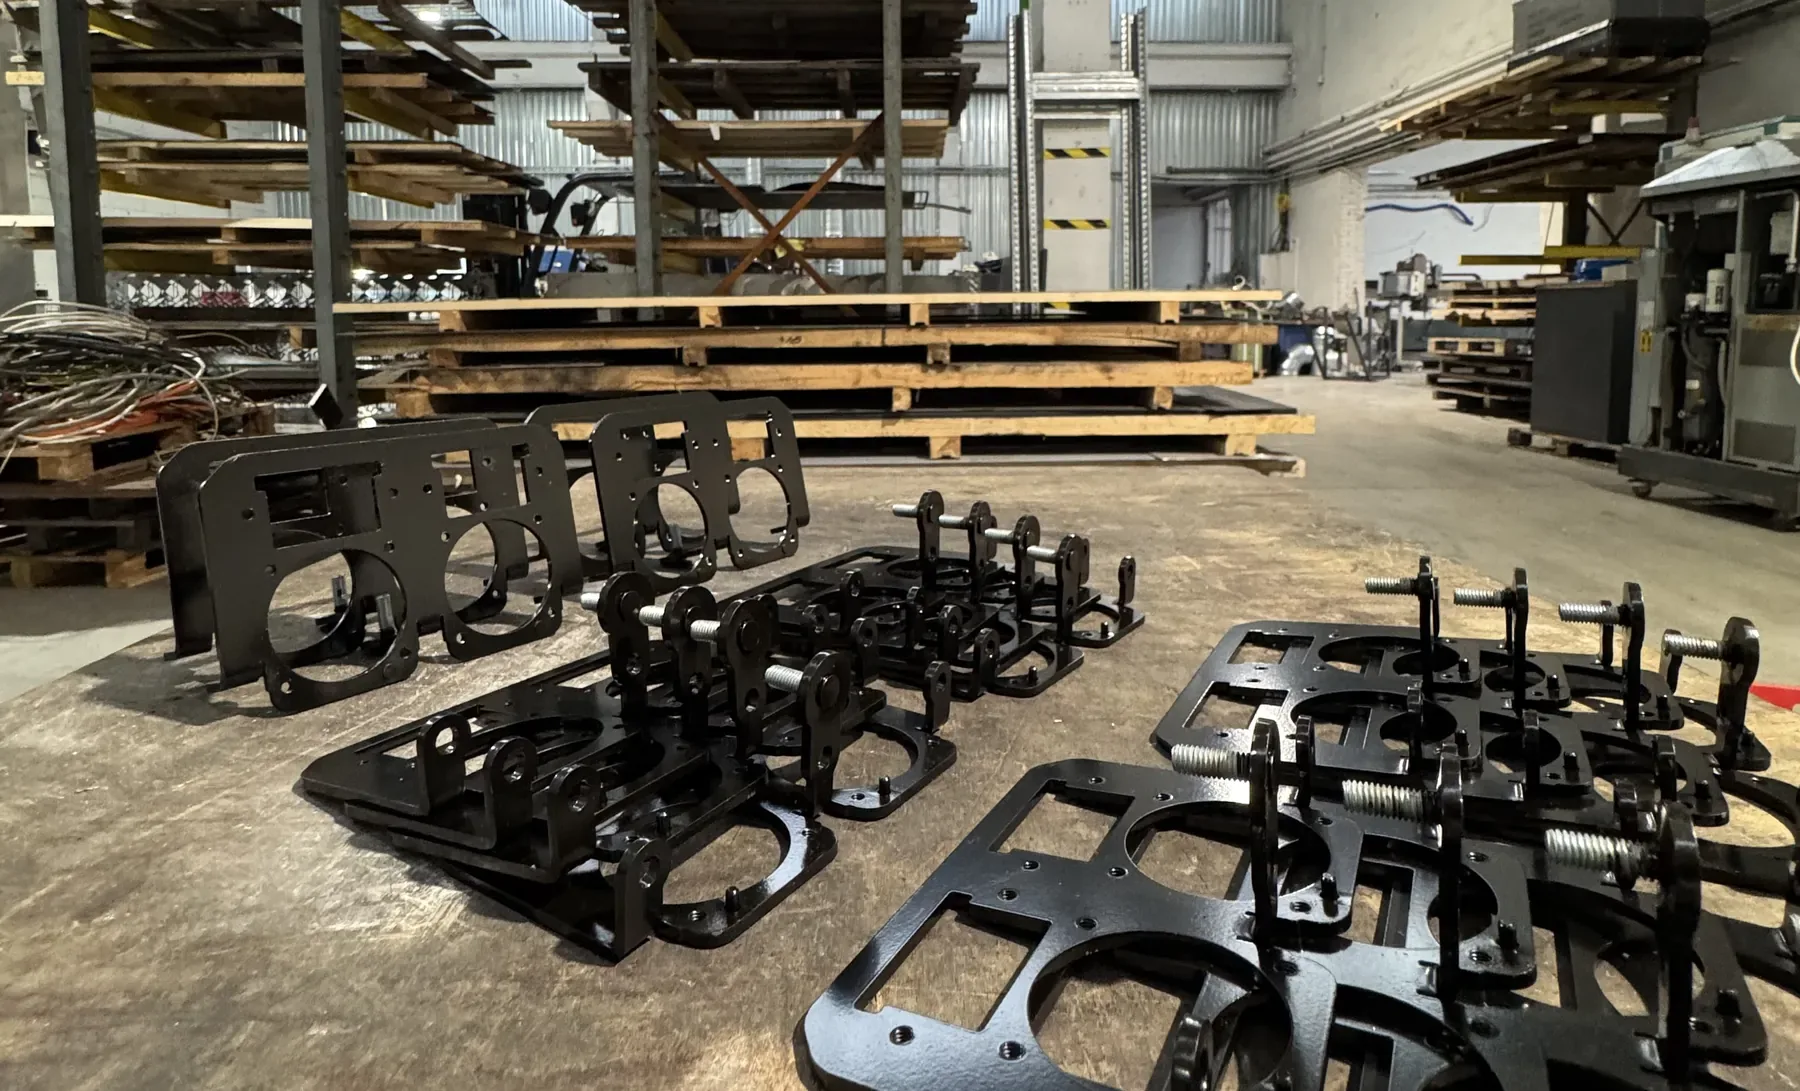
Bending a part in press brake tooling. ECAD shop floor. Batch of bent sheet metal parts on pallets. ECAD shop floor. Bent sheet metal profiles. ECAD shop floor. Bent sheet metal parts on a table.
How to order sheet metal bending
We quote sheet metal bending services based on a 3D model or technical documentation, not from a price list. Ideally, send a model or drawing with dimensions, bend angles and bend radii. More: what determines the price of cutting and bending. Guide: how to prepare a file for laser cutting and bending.
The price depends on:
- material and material thickness
- bending length
- number of bends per part
- quantity
- cutting and deburring the blank
- welding and lead time
Send a drawing or 3D model
PDF, DXF, DWG, STEP, IGES, photos (JPG, PNG, TIFF) or a ZIP or 7Z archive. Up to 10 files, up to 100 MB in total.
Describe your order
Material and grade, material thickness, quantity, lead time, and whether we should also cut the blank.
We will reply with any questions and a price
We will send a quote or ask for any missing details.
We process enquiry data in accordance with our privacy policy.
Questions about sheet metal bending
Do you offer custom sheet metal bending from a single piece?
Yes. We carry out custom sheet metal bending from one-off parts to series production, based on a drawing or 3D model.
What length of sheet metal can be bent?
The TruBend 7050 bends lengths up to 1530 mm. A second press brake, the Trumpf TruBend 3130 with a bending length of 3230 mm, will join our fleet soon.
What sheet metal thickness can the press brake bend?
As a guide: over the full 1530 mm length, the TruBend 7050 (500 kN) bends structural steel up to approx. 4 mm thick, and thicker sheet metal over shorter lengths, e.g. 6 mm up to approx. 1080 mm. Details are in the bending table; we confirm this for your specific part when preparing the quote.
How much does sheet metal bending cost?
We do not have a fixed price list. We prepare quotes based on a model or technical documentation. The price depends on the material, material thickness, number of bends, quantity and additional operations. See cutting and bending price list: what determines the price.
Can you cut the sheet metal before bending?
Yes. We cut the blank on a 12 kW laser, deburr it and bend it within a single order. See sheet metal laser cutting.
Do you also bend tubes and profiles?
Yes, on a VLB EB53CNC-RH CNC mandrel tube bender. See tube and profile bending.
Sheet metal folding and forming: is that the same as bending?
Yes. In Polish, these are everyday terms for bending on a press brake. At ECAD, we bend on a Trumpf TruBend 7050 press brake, from one-off parts to series production, from a drawing or 3D model.
Have a drawing?
Send your file and tell us what you need: material, material thickness, quantity and number of bends. We will reply with any questions and a price.


